An industrial pressure vessel may reach the design-life assumption specified in its original project without automatically becoming unfit for service. Another vessel can develop unacceptable damage long before that assumption is reached. Neither the age of the vessel nor the design-life number on a datasheet is, by itself, permission to continue operating—or an automatic instruction to replace the equipment.
For plant owners and EPC replacement-project buyers, the useful question is more specific: What was the vessel designed to withstand, what has it actually experienced, what is its present condition, and what evidence is needed to justify continued service or a new equipment specification?
The answer requires a distinction between the original design basis, elapsed service, damage-specific remaining-life estimates, and a formally approved repair, rerating, or replacement decision. This article explains how to organize those inputs and carry lessons from the existing vessel into procurement of a complete industrial pressure vessel. It does not calculate a remaining safe life or authorize continued operation of a particular item.
What Is the Difference Between Design Life, Service Life and Remaining Life?
The word life can refer to several different engineering concepts. Treating them as interchangeable can lead to incorrect purchase specifications and unsupported operating decisions.
| Term | What it describes | What it does not prove |
|---|---|---|
| Design life | The specified planning horizon or duty assumption used in developing the equipment's design basis, which may involve operating years, cycles, or other defined conditions | That the equipment will remain safe for that duration regardless of damage, or must automatically be scrapped when the period ends |
| Elapsed service life | How long the vessel has actually been in service, with the relevant operating and outage history | Its current structural condition or remaining usable life |
| Assessed remaining life | A qualified, mechanism-specific projection or evaluation based on the present condition, expected future service, and the selected methodology | A universal number independent of corrosion, cracking, fatigue, inspection quality, or changes in service |
| Inspection planning horizon | The period or conditions established by an authorized inspection program for its next review | A guarantee that the vessel is free from all degradation until that date |
| Replacement timing | A project decision based on integrity findings, required future service, approved repair or rerating options, risk, and lifecycle planning | A fixed anniversary derived from the original purchase date |
These are procurement-oriented descriptions, not definitions reproduced from a proprietary standard. The governing regulations, contract and approved engineering procedure control the actual decision.
Design life is a documented assumption, not a universal expiry date
A vessel's original design may account for a specified operating duty, fluid, pressure and temperature range, expected corrosion behavior, and—where applicable—pressure or temperature cycling. Different damage mechanisms require different evidence and design or assessment approaches. A nominal design-life period should therefore be read alongside the actual assumptions that supported it.
Buyers should ask what the design-life statement was intended to cover: a project planning requirement, an allowance for corrosion under defined conditions, an assessed cyclic duty, or another documented design basis. Not every pressure vessel has the same explicitly stated lifecycle assumptions, and an unsupported life claim should not be created retroactively.
The broader site's pressure vessel service-life guide explains why vessel longevity varies with service. Here, the emphasis is on documenting the assumptions and evidence needed for the next engineering or procurement decision.
Elapsed years cannot establish remaining life
A vessel's commissioning date may be well documented even when its corrosion rate, operating cycles or material condition are not. Age remains relevant to record retrieval and inspection planning, but it does not substitute for condition evidence.
A relatively recent vessel may have experienced severe localized corrosion or unexpected cycling. An older vessel may have a useful history of stable operation and inspection. Neither description is an accept-or-reject conclusion: the owner needs the applicable technical assessment.
Remaining life has to be tied to the limiting concern
A projection based on measured general wall thinning addresses one potential limit; it does not automatically resolve crack-like damage, high-temperature degradation, hydrogen damage or fatigue. Different components and locations can also have different limiting conditions.
An acceptable record should explain what life is being estimated against, which data and assumptions were used, and what uncertainty remains. If key inspection records or the mechanism-specific basis are missing, the correct procurement entry is unresolved, not a guessed number of safe years.
Why Can a Vessel Reach Its Design Life Without Requiring Immediate Replacement?
Whether a pressure vessel can continue in its intended service is an engineering and regulatory matter, not a simple subtraction of calendar years from an original target.
The American Petroleum Institute's API 510 overview identifies an in-service framework covering inspection, rating, repair, and alteration of applicable pressure vessels. The ASME description of API 579-1/ASME FFS-1 explains how a multidisciplinary fitness-for-service (FFS) assessment may be used for pressure equipment containing flaws, damage or aging-related concerns.
These sources demonstrate why actual condition and approved assessment methods matter. They do not create an automatic worldwide extension when a design-life assumption has been reached.
Three different questions must be answered
1. Is the original design basis still relevant? The process medium, contaminants, maximum and normal operating conditions, cycling, and intended future duty may have changed. A design adequate for a previous service cannot simply be assumed suitable for a new one.
2. Is the equipment's present condition sufficiently established? The answer depends on inspection coverage and effectiveness, repair history, material traceability, credible damage mechanisms, and the ability to evaluate relevant defects.
3. Do the governing rules and authorized decision makers permit the proposed course? Local law, the project's in-service inspection framework, owner requirements and a qualified assessment may constrain the available choices.
Do not mistake an FFS evaluation for a blanket extension
A fitness-for-service assessment is specific to the component, identified damage, available evidence, evaluation method and proposed operating conditions. It can support an informed run, repair, rerate or replace decision within its authorized scope, but it is not an unconditional guarantee for a different future service.
Similarly, an accepted repair is not proof that the original damage mechanism has disappeared. A repaired area and its surrounding components may still require appropriate examination and monitoring, and the cause of deterioration must be reviewed.
A younger vessel may still require action
Serious cracking, unanticipated metal loss, deformation, overtemperature exposure or another significant integrity concern can require an earlier decision than the nominal project design-life date. Suspected dangerous conditions must be escalated through the facility's established safety and mechanical-integrity process; this article does not prescribe operating or shutdown actions.
What Inspection and Operating Evidence Is Needed to Assess Remaining Life?
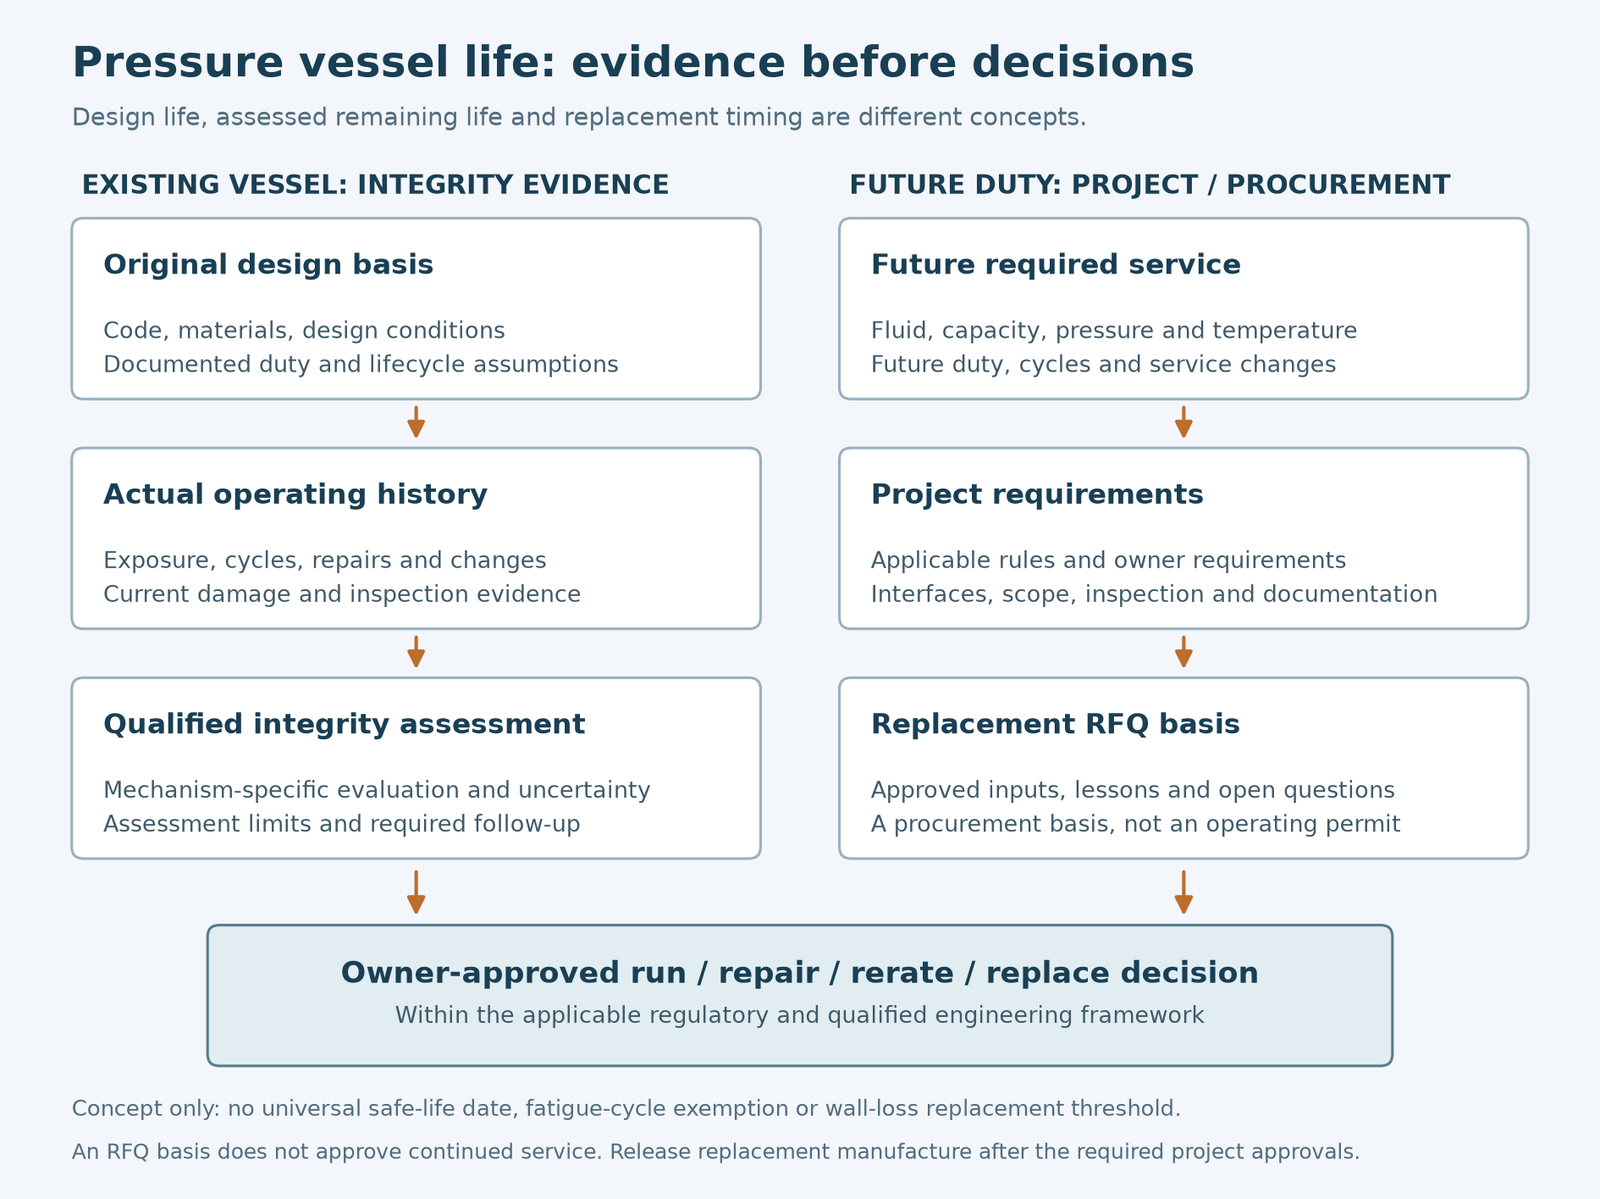
An assessment package should connect three evidence sets: the original equipment, what happened during service, and what has been verified about current condition. The exact scope must be set by competent inspectors, materials specialists and engineers.
Retrieve the original construction and design record
Useful records may include:
- Vessel identification, serial number, manufacturer, year and applicable construction code and edition.
- Approved drawings, vessel configuration, dimensions and relevant component details.
- Original design pressure and temperature, operating assumptions and intended design duty.
- Materials of construction, corrosion allowance or other protection strategy, and material traceability.
- Relevant fabrication, welding, heat-treatment, examination and test documentation.
- Any design assessment involving cyclic loading or elevated-temperature service, where applicable.
- Previous changes to pressure rating, service or configuration.
A document labeled “design life” should be read in context rather than detached from the assumptions or engineering calculations it references.
Reconstruct the actual operating and repair history
The owner may need to obtain evidence of:
- Actual process fluids, chemical composition and contaminant variations.
- Pressure and temperature trends, including significant deviations where recorded.
- Startup, shutdown and other relevant thermal or pressure cycles.
- Changes in throughput, concentration, chemistry or operating regime.
- Known leaks, corrosion events, damage investigations and abnormal events.
- Previous repairs, alterations, reratings and related approvals.
- Protective-system and maintenance history to the extent relevant to the assessment.
The data should distinguish documented measurements from reconstructed or assumed operating cases. Missing historical information should be recorded as a limitation, especially when it could materially affect the selected damage assessment.
Match inspection methods to the damage mechanism
| Potential concern | Evidence that may be relevant | Important limitation |
|---|---|---|
| General metal loss | Traceable thickness measurements at representative locations and a justified trend | Measurements do not automatically reveal localized or crack-like damage |
| Localized corrosion or pitting | Suitable examination coverage and characterization of affected locations | Sparse measurements may miss the governing local defect |
| Fatigue or thermal-cycle damage | Relevant stress and cycle history, component details, and suitable flaw examination | Calendar age and an arbitrary cycle cutoff are insufficient |
| Stress corrosion cracking or hydrogen-related damage | Service-specific materials assessment and appropriate inspection | General thickness stability does not exclude these mechanisms |
| Elevated-temperature degradation | Actual temperature/exposure history, materials and specialist assessment | A single nominal operating temperature is inadequate |
| Repair or alteration condition | Repair records, method and examination evidence, and continuing service conditions | A documented repair does not by itself demonstrate remaining life |
The inspection approach and evaluation acceptance criteria must be determined for the actual vessel and governing framework.
A thickness trend can be important where predictable general corrosion is the limiting mechanism. But a wall-thinning-based life estimate cannot be presented as the remaining life for the entire vessel when another credible mechanism may govern.
What if inspection records are incomplete?
The appropriate next step is a gap assessment by the owner's authorized team. It may identify the need for further inspection, engineering reconstruction, more conservative assumptions, or restrictions pending clarification. The outcome cannot be predetermined by a general purchasing article.
A missing corrosion trend, undocumented historical repairs, or uncertain material identity should be flagged explicitly in the condition register. Do not replace missing measurements with an assumed corrosion rate or an invented service-life number.
How Do Damage Mechanisms, Cycling and Process Changes Affect the Decision?
Pressure-vessel life is not controlled by one degradation mechanism in every service. The evidence required for evaluation changes with the credible threats to the vessel and its components.
Metal loss does not cover every type of damage
Corrosion or erosion may gradually reduce wall thickness. Some services can also produce localized corrosion, damage beneath deposits, or deterioration at specific geometric locations. Evaluation may depend on the location and nature of damage, the required minimum thickness or strength, and the rate at which damage is progressing.
An “x percent wall loss” rule cannot be substituted for the relevant engineering assessment. An identical percentage of metal loss may have different significance for different equipment, materials, geometry and local conditions.
Pressure and temperature cycles require a suitable engineering basis
Fatigue concerns depend on more than the number of startup or pressure cycles. Relevant factors can include stress range, geometry, weld details, temperature gradients, sequence, and applicable fatigue design or reassessment methodology.
There is no sound procurement basis for a universal statement that fewer than 10,000 cycles make fatigue negligible. Nor should a design-life claim imply that all vessels undergo the same fatigue assessment. The responsible engineer must determine whether cyclic loading is relevant and what evidence is needed.
Temperature and chemistry changes can alter the controlling mechanism
A service change can introduce a damage mechanism that was not part of the original design assumptions. Examples include more aggressive contaminants, higher temperature, a different hydrogen exposure, or changes in the liquid composition. The engineering team may need to revisit material compatibility, design limits and inspection strategy before making a remaining-life decision.
Repairs and alterations require an updated baseline
If the vessel has been repaired or altered, the integrity review should establish what changed, the applicable approval basis, and whether the original cause of damage has been addressed. The ASME PCC-2 description identifies repair methods for in-service pressure equipment, but such methods follow appropriate inspection and flaw evaluation rather than replace it.
An approved repair may change the relevant condition of a component. It does not automatically restore the whole vessel to its original design-life assumption or reset every degradation process to zero.
Keep inspection planning separate from a lifespan claim
The owner should operate under the applicable in-service framework and a justified inspection plan that addresses the relevant equipment and damage mechanisms. In Great Britain, the Health and Safety Executive's INDG178(rev2), published in 2012, explains written schemes of examination under the Pressure Systems Safety Regulations 2000. Its requirements and terminology are jurisdiction-specific, not universal international rules.
For more detailed consideration of inspection intervals and examination methods, see the site's pressure vessel inspection-frequency guide. This article does not reproduce generic inspection schedules or claim that ASME BPVC itself imposes a single fixed worldwide inspection interval.
When Should an Owner Consider Repair, Rerating or Full Replacement?
An integrity finding and a procurement decision are related but not identical. A vessel may be technically repairable while replacement is still preferred because of future service requirements, recurring degradation or project execution constraints. Conversely, a nominated replacement date should not be treated as evidence that an existing vessel has failed.
Use a qualified decision matrix
| Engineering finding or project condition | Main review question | Possible project outcome |
|---|---|---|
| Documented condition supports intended service under approved assessment | Are operating conditions, inspection requirements and approvals adequately controlled? | Continued service under the authorized integrity program |
| Localized damage with an approved repair approach | Is repair technically suitable, and has the damage cause been addressed? | Repair and reassessment as required |
| Current rating no longer aligns with condition or required service | Is a revised allowable service condition technically and legally acceptable? | Engineering rerating review |
| Extensive, recurring or poorly characterized degradation | Can integrity be established with sufficient confidence and acceptable lifecycle consequences? | Major rehabilitation or full replacement evaluation |
| New process duty exceeds the documented original basis | Can the existing vessel be reassessed and modified within requirements? | Modify, rerate or procure a new vessel |
| Rising inspection and maintenance burden | Is keeping the existing item the best technically acceptable lifecycle option? | Compare accepted repair and replacement proposals |
These are decision routes, not predetermined approvals or operational instructions.
A proper comparison considers the applicable integrity requirements first. Only technically acceptable options should move into project cost, outage and schedule comparisons.
What should the engineering approval actually say?
A useful owner-side decision record should identify:
- The equipment and service conditions covered.
- The inspected condition, observed damage and assessment limits.
- The accepted or rejected engineering options and their technical basis.
- Required follow-up examination, restrictions or monitoring, if applicable.
- The authorized decision maker, approval date and document revision.
- The future duty assumed when deciding to repair, rerate or replace.
If a separate, future service is proposed, the engineering review must address that change rather than extrapolate an old approval uncritically.
Why replacement planning may begin before a final retirement decision
Long-lead equipment, outage coordination and project design work may justify starting procurement studies while the integrity decision is still being completed. Buyers can request a budgetary replacement proposal with clearly labeled provisional inputs.
However, such commercial planning is not permission to continue operating a potentially compromised vessel. The owner's competent integrity team remains responsible for the assessment and authorized operating decision.
What Should EPC Buyers Transfer Into a New Pressure Vessel RFQ?
Once replacement is being evaluated, the lessons from the existing equipment should inform the new vessel's design basis. Simply copying the original datasheet can reproduce the same material vulnerability or omit changed process requirements.
Build a lifecycle-informed procurement register
| RFQ field | Evidence or specification required | Responsible source or reviewer |
|---|---|---|
| Future service and process medium | Actual intended fluids, composition, contaminants and variability | Owner / process engineer |
| Capacity and operating duty | Required inventory or throughput, working range and credible operating cases | Owner / EPC process team |
| Pressure and temperature design basis | Approved normal, design and relevant transient conditions | Process and mechanical design authorities |
| Expected cycles and lifecycle assumptions | Approved pressure/temperature cycling basis and specified planning horizon | Process / mechanical engineering |
| Damage mechanisms from the existing vessel | Confirmed degradation mechanisms, uncertainty and investigation results | Owner integrity / materials specialists |
| Material and corrosion strategy | Approved materials basis and relevant protective or corrosion allowances | Materials and mechanical engineering |
| Mechanical configuration | Orientation, supports, nozzles, interfaces and approved design loads | EPC and mechanical engineering |
| Inspection and maintainability | Access provisions and applicable examination or maintenance interfaces | Owner inspection team / designer |
| Codes and destination | Applicable construction code edition, local rules and contractual verification requirements | Owner / EPC compliance team |
| Documentation deliverables | Drawings, material records, weld/NDE documentation, reports and agreed quality records | EPC quality team / manufacturer |
| Existing-equipment removal and site works | Boundaries with civil, lifting, piping and installation contractors | EPC / project execution team |
| Critical unresolved issues | Missing evidence, provisional assumptions and mandatory approvals | Named issue owner and closing authority |
This is an editorial handover template for industrial equipment procurement, not a prescribed code form.
For large industrial storage-tank replacement projects, this article discusses 10 m³ and above equipment only. The manufacturer's industrial storage-tank product page describes a wider custom manufacturing portfolio; that page does not mean every in-service integrity assessment or future-duty suitability review is included in the manufacturing contract.
Separate the owner's assessment from the supplier's manufacturing commitment
Owner and operator: Maintain reliable service history, address immediate integrity concerns through established procedures, and approve the decision about the existing vessel.
Qualified inspector, materials and integrity engineers: Evaluate the actual condition and damage mechanisms, interpret relevant inspection results, and recommend appropriately supported options under their assigned authority.
EPC process and mechanical engineers: Establish the new service basis, engineering interfaces, applicable standards and project-specific lifecycle assumptions.
Vessel manufacturer: Review the approved fabrication and mechanical design specification, explain the offered manufacturing and documentation scope, and identify deviations requiring clarification.
The manufacturer should not be assumed to provide a full fitness-for-service assessment, continuing-operation authorization, or plant-wide integrity program unless separately verified and expressly contracted.
Do not copy an old life estimate into the new purchase order
A previous remaining-life projection describes an existing vessel under specified assessment conditions. A new vessel requires its own approved design basis, materials, corrosion strategy and—where applicable—cycling assumptions. The old assessment is useful as a record of what the previous equipment experienced, not as an automatic design guarantee for the replacement.
For a technical enquiry about a complete industrial vessel, submit the intended medium, relevant composition, capacity, pressure/temperature range, cycling conditions, required code, project location, material constraints and the engineering findings that explain why a new unit is being considered.
Frequently Asked Questions
Does reaching the design life automatically mean that a pressure vessel must be replaced?
Not automatically. Design life is a documented design assumption or requirement, not a universal scrap date. Continued service depends on the actual condition, future service, applicable regulations, inspection program and authorized engineering assessment. Some equipment may require action before that date; other equipment may be evaluated for continued service under the applicable framework.
Can vessel age alone establish remaining life?
No. Age does not identify wall loss, cracking, fatigue usage or other damage. A defensible remaining-life assessment needs evidence suited to the relevant mechanism, not merely a commissioning date.
Is measured wall thickness enough to determine remaining life?
Not for every vessel. Thickness data can inform evaluations involving material loss, but they do not necessarily characterize fatigue cracks, stress corrosion cracking, creep, hydrogen damage or other mechanisms. The responsible specialist must establish the assessment scope and data adequacy.
Does an ASME pressure vessel have a universal inspection or replacement interval?
No universal international interval follows merely from describing a vessel as ASME-designed. In-service inspection and continued operation depend on the applicable jurisdiction, owner program, service conditions and adopted inspection framework. See the separate inspection-frequency article for a detailed discussion.
Can a repaired vessel regain its original design life?
Not automatically. The significance of a repair depends on the actual damage, repair design, examination, remaining degradation risks and applicable engineering approval. A repair record is one input to—not a substitute for—a new assessment.
What should buyers provide before ordering a replacement pressure vessel?
At minimum, provide an approved future service description, relevant pressure and temperature conditions, fluid composition, intended duty, applicable code and jurisdiction, and design/inspection documentation requirements. Where the existing vessel's problems affect the new design, provide the owner-approved damage findings and material or maintainability lessons without presenting unresolved hypotheses as facts.
Conclusion
Industrial pressure vessel design life, elapsed service and assessed remaining life are separate concepts. None is a universal, stand-alone authorization to operate or a mandatory calendar-based replacement trigger.
For existing equipment, the owner must establish what the original design assumed, what the vessel actually experienced, what damage is present and which assessment method is appropriate. The resulting integrity decision belongs to qualified and authorized personnel under the applicable framework.
For replacement projects, the most valuable outcome is a controlled transfer of evidence: current process duty, damage mechanism, future operating conditions, cyclic requirements, materials basis, inspection access and documentation. That gives EPC buyers and equipment manufacturers a better foundation for a complete-vessel specification without relying on arbitrary lifespan rules or unsupported guarantees.
References
- American Petroleum Institute (API). New Edition of API 510 Enhances Safety of Pressure Vessel Inspection Code. Official description of API 510's in-service inspection, rating, repair and alteration scope. https://www.api.org/products-and-services/standards/important-standards-announcements/tradeannouncement-api510
- American Society of Mechanical Engineers (ASME). API 579-1/ASME FFS-1 Fitness-For-Service — Course Overview. Public explanation of multidisciplinary FFS assessment for damaged or aged pressure equipment; not a reproduction of the standard. https://www.asme.org/learning-development/find-course/api-579-1-asme-ffs-1-fitness-service-evaluation
- UK Health and Safety Executive (HSE). (2012). Written Schemes of Examination, INDG178(rev2). Guidance under the Pressure Systems Safety Regulations 2000 in Great Britain; not a worldwide inspection schedule. https://www.hse.gov.uk/pubns/indg178.htm
- HSE. Pressure Systems Safety Regulations 2000 (PSSR). Public explanation of the owner/user and competent-person responsibilities within the applicable UK regime. https://www.hse.gov.uk/pressure-systems/pssr.htm
- ASME. PCC-2 — Repair of Pressure Equipment and Piping. Publisher's overview of repair practices for relevant pressure equipment after appropriate inspection and flaw assessment. https://www.asme.org/codes-standards/find-codes-standards/repair-of-pressure-equipment-and-piping
- API. API RP 572, Inspection Practices for Pressure Vessels — Fifth Edition Announcement. Publisher overview of inspection practice, examination methods and records, supplementing the API 510 framework. https://www.api.org/products-and-services/standards/important-standards-announcements/rp572-tradepress