A chemical plant may have sufficient steam generation capacity over an entire production cycle and still experience pressure problems during short periods of high demand. For projects considering an industrial steam accumulator, identifying the highest instantaneous steam flow is only the beginning of the engineering assessment.
Before sizing an industrial steam accumulator, buyers should prepare a time-stamped steam-demand profile that identifies peak flow, peak duration, simultaneous steam consumers, available supply, repeated operating cycles and recharge windows. The profile must also be evaluated against the charging and discharge pressure conditions, rather than using peak demand alone to select vessel volume.
This information helps process engineers and EPC buyers determine whether thermal storage can address a temporary steam deficit and what technical evidence an equipment supplier needs before proposing a complete pressure vessel.
Why Is Peak Steam Flow Alone Insufficient for Accumulator Sizing?
The maximum instantaneous steam flow does not describe how much stored energy the plant requires or how quickly that energy must be released.
A conventional pressure-drop steam accumulator stores thermal energy primarily in pressurized hot water. During charging, incoming steam transfers energy to the stored water. During discharge, a controlled pressure reduction causes part of that water to flash into steam.
The useful output depends on the permitted pressure range and the operating conditions of the complete system.
Peak Magnitude and Duration Answer Different Questions
Consider two hypothetical process demands that reach the same maximum flow:
- One process reaches its peak briefly during equipment startup.
- Another maintains the same peak throughout a longer batch-heating operation.
The required stored-energy contribution can be substantially different, even if the maximum flowrates are identical.
The demand profile must therefore identify both the magnitude and duration of the steam requirement.
A supplier also needs to know what the existing supply system can deliver during each peak. If steam generation continues to meet part of the process demand, the accumulator only needs to contribute the remaining required flow, subject to actual system limitations.
Repeated Peaks Change the Assessment
The profile must extend beyond a single isolated peak.
If two batches require additional steam within a short interval, the accumulator may begin the second event in a partially charged condition.
A capacity estimate based only on the first peak could therefore overstate the energy available for the second.
Spirax Sarco’s steam accumulator engineering guide explains the importance of overload periods, off-peak steam availability and the time required for recharging.
An accumulator cannot compensate indefinitely for a sustained shortage of steam generation. It shifts energy between periods with different demand and supply conditions. Before requesting a vessel quotation, the project team should establish that suitable charging opportunities exist.
What Data Should a Steam-Demand Profile Record?
A steam-demand profile should show how consumption changes over time, under identifiable process conditions.
A single daily total, average steam consumption value or list of equipment nameplate ratings cannot describe all the information needed for accumulator assessment.
Prepare a Time-Stamped Record
The following fields provide a practical starting point for process data collection.
| Record field | Information to provide | Why it matters |
|---|---|---|
| Timestamp and interval | Beginning and end of each observation, time zone and recording interval | Establishes when demand occurs and how long it lasts |
| Steam mass flow | Measured or calculated steam flow, with consistent units such as kg/h | Quantifies the load during each interval |
| Steam pressure | Pressure value and measurement location | Establishes the pressure conditions associated with consumption |
| Steam temperature | Recorded or specified temperature, with relevant measurement basis | Supports the steam-state and energy assessment |
| Steam condition | Saturated or superheated condition, with applicable quality information | Helps establish the appropriate thermodynamic basis |
| Production equipment | Equipment identification and operating status | Connects steam demand to actual process activities |
| Batch or operating phase | Startup, heating, holding, cleaning, standby or another defined phase | Identifies why demand changes |
| Simultaneous consumers | Other equipment operating during the same period | Supports calculation of the combined plant load |
| Data origin | Measured, calculated, inferred or estimated | Separates evidence from design assumptions |
| Data quality | Meter limits, missing observations, uncertainty and unusual events | Prevents unreliable values from being treated as verified inputs |
| Cycle identification | Shift, batch, daily or weekly schedule | Allows repeated duty patterns to be compared |
Editorial steam-demand recording template; not a prescribed instrument specification or regulatory form.
For existing facilities, suitably located steam flowmeters and historical operating records may provide useful information.
Spirax Sarco’s measurement of steam consumption guidance discusses steam flow measurement and methods for establishing consumption over time.
Choose a Time Interval That Preserves the Peaks
The recording interval should be short enough to capture the relevant transient demand.
An hourly consumption average can conceal a steam peak lasting only several minutes. Even a shorter interval may be inadequate if the process contains faster events.
The appropriate interval depends on the plant’s operating pattern, available instrumentation and the transient behavior that must be evaluated.
Buyers should document whether values are instantaneous readings, averages over a period or integrated totals converted into average flowrates.
These quantities should not be mixed without identifying their measurement basis.
Distinguish Measured and Estimated Loads
For a plant that has not yet been commissioned, actual steam-demand measurements may not exist.
The process engineering team may estimate consumption from equipment heat duties, operating schedules and appropriate steam enthalpy differences.
The Spirax Sarco guide to estimating steam consumption distinguishes process calculations, measurements and equipment thermal ratings.
The resulting load profile should identify which points are estimates, the assumptions behind them and which values still require validation.
An equipment nameplate rating should not automatically be used as its actual steam consumption throughout the production cycle.
How Should Overlapping Peaks and Repeated Load Cycles Be Analyzed?
A plant’s peak steam demand depends on the timing of its consumers, not merely on the sum of their individual maximum ratings.
This distinction is especially important for chemical plants with batch production, intermittent heating and equipment startup sequences.
Identify Coincident Steam Loads
The engineering team should review the schedule of major steam consumers, including:
- When each consumer starts and stops.
- When its highest steam demand occurs.
- Whether two or more high-demand phases can overlap.
- Whether the operating sequence changes between shifts or product batches.
- Whether simultaneous demand is restricted by production controls or operator procedures.
If two batch vessels begin heating at the same time, their combined demand may produce a peak that does not appear in either equipment’s individual average consumption.
Conversely, equipment that operates in mutually exclusive production stages should not automatically have its nameplate maximum loads added together as though all peaks occur simultaneously.
The combined profile should reflect credible operating combinations.
Record the Complete Repeating Cycle
For each important cycle, identify the sequence of demand peaks and lower-load periods.
The record should extend long enough to capture the relevant repetition, including successive batches, shift changes and other operating modes where applicable.
Buyers should distinguish between a typical production day and a credible limiting operating scenario.
A single favorable test run may not represent the most demanding repeated schedule.
Check the Initial Condition Before Each Peak
The state of the accumulator at the beginning of a peak affects its ability to provide additional steam.
A vessel that starts fully charged may satisfy an isolated event, while the same vessel could fail to support a similar event if insufficient recharge occurred after the previous discharge.
For that reason, the repeated cycle should be assessed as a connected sequence rather than as independent maximum-flow events.
Where the plant has no historical records, an assumed batch schedule should be provided and clearly labeled as a process design scenario.
How Should Steam Demand Be Compared With Available Supply Over Time?
Once the steam-demand profile is prepared, it should be compared with the steam actually available to serve the relevant process boundary.
The available supply must be defined consistently with the demand.
Boiler nameplate capacity alone may not represent the steam that can be delivered during each interval, particularly when other consumers, operating restrictions, pressure limitations or response characteristics apply.
Identify Deficit and Potential Recharge Periods
For a preliminary review, the instantaneous steam-mass-flow deficit may be written as:
Deficit mass flow(t) = max[0, demand mass flow(t) − available mass flow(t)]
For each time interval, the nominal steam-mass shortfall can be estimated from the average deficit flow multiplied by the duration.
The same comparison can identify periods during which available supply exceeds demand.
However, a nominal surplus does not automatically represent steam that can actually be transferred into the accumulator. The charging pressure, equipment condition, connection capacity and control arrangement must also permit that transfer.
Illustrative Short-Cycle Demand Profile
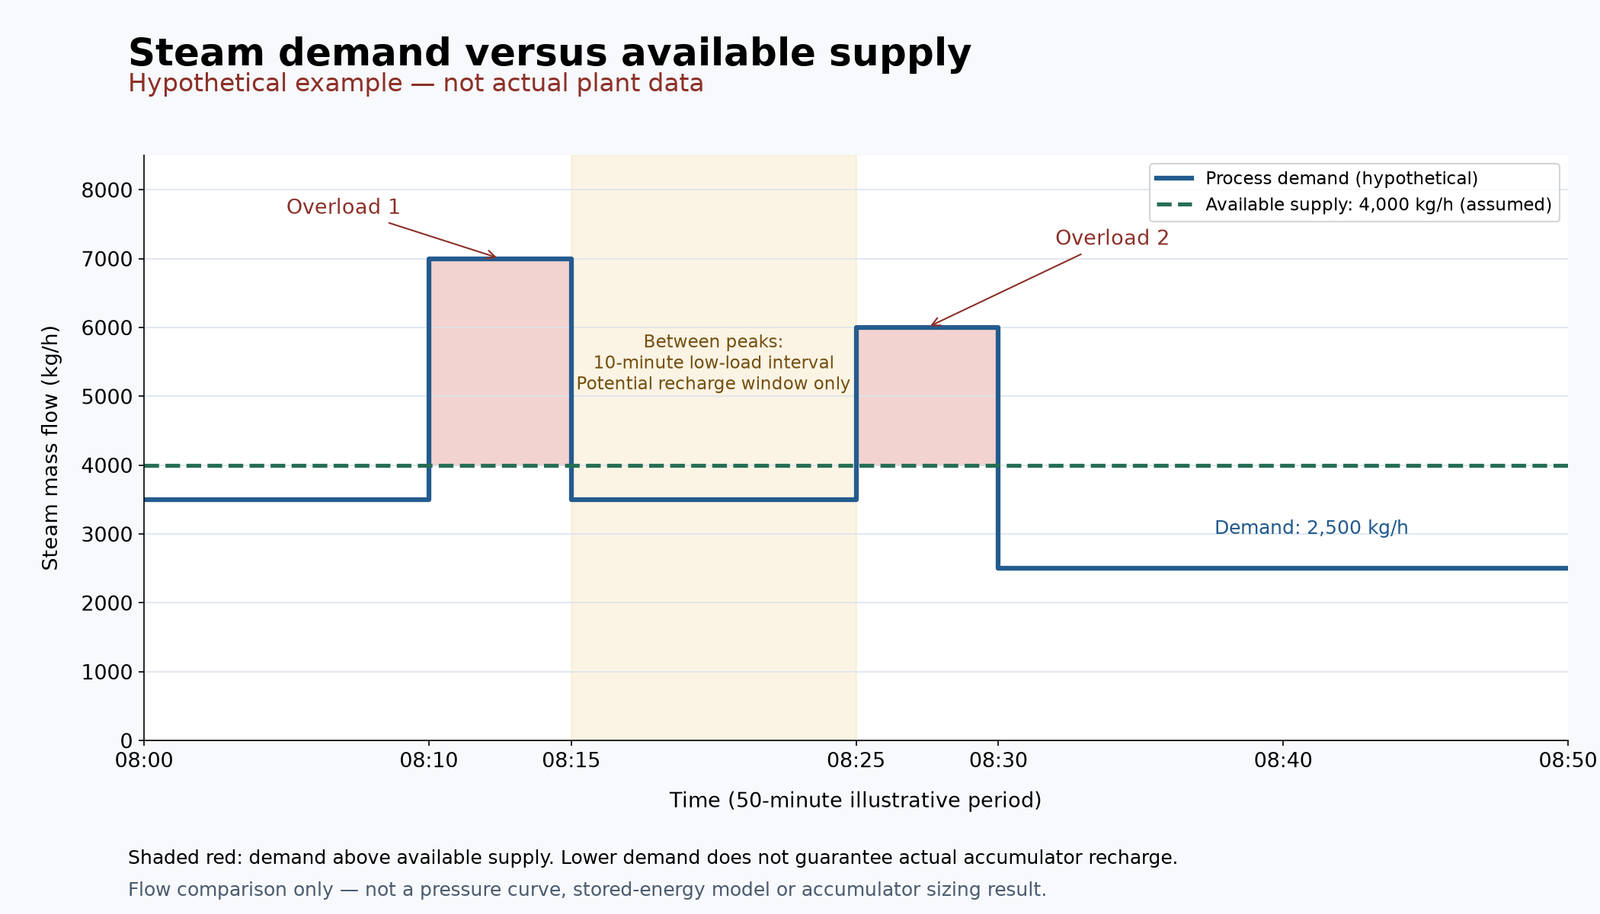
Assume an industrial plant has 4,000 kg/h of steam available at the selected comparison boundary throughout a hypothetical 50-minute production period.
The table illustrates how demand changes during that period.
| Time interval | Process demand | Difference from available supply | Nominal steam-mass difference |
|---|---|---|---|
| 08:00–08:10 | 3,500 kg/h | 500 kg/h surplus | 83 kg potential surplus |
| 08:10–08:15 | 7,000 kg/h | 3,000 kg/h deficit | 250 kg shortfall |
| 08:15–08:25 | 3,500 kg/h | 500 kg/h surplus | 83 kg potential surplus |
| 08:25–08:30 | 6,000 kg/h | 2,000 kg/h deficit | 167 kg shortfall |
| 08:30–08:50 | 2,500 kg/h | 1,500 kg/h surplus | 500 kg potential surplus |
Hypothetical illustration only. All values are assumed, not measured plant data or a company project reference. Mass differences are rounded.
Across the full 50 minutes, the average demand is 3,700 kg/h, below the assumed 4,000 kg/h available supply.
Nevertheless, the schedule contains two overload periods. The interval between them provides only a limited potential opportunity for recharging.
Why the Steam-Mass Shortfall Is Not Vessel Capacity
The hypothetical deficit values describe a preliminary flow mismatch over time.
They do not directly determine:
- The required quantity of pressurized stored water.
- The accumulator’s geometric vessel volume.
- The flash-steam capacity at the allowed pressure range.
- The actual charging time or transfer capability.
- The final steam-discharge performance.
Those results require a suitable thermodynamic and equipment assessment.
For example, the steam used to charge the accumulator transfers energy to pressurized water. It should not be assumed that one kilogram of charging steam produces exactly one kilogram of useful flash steam during a later discharge.
The preliminary time-series comparison identifies what must be evaluated; it does not replace the final accumulator sizing calculations.
How Should Recharge Windows and the Usable Pressure Range Be Checked?
A steam-demand assessment should confirm that the accumulator can recover sufficiently after discharge and before the next important demand peak.
A low-demand interval is only a potential recharge window. Its actual usefulness depends on available steam conditions and the state of the accumulator.
Review the Available Recharge Window
For every repeated peak sequence, the process engineering team should establish:
- The end of the preceding discharge event.
- The start of the next expected overload.
- The actual steam available for charging during the intervening period.
- Applicable pressure and flow restrictions.
- The required accumulator condition before the next discharge.
The available charging rate may change as accumulator pressure increases.
Therefore, the calculation should not assume a constant maximum charging flow unless that assumption is supported by the proposed equipment and operating conditions.
Spirax Sarco’s steam accumulator guide evaluates both the available off-peak steam and the time required to recharge a pressure-drop accumulator.
Verify the Pressure Window
For the conventional pressure-drop accumulator discussed here, the following conditions should be distinguished:
| Pressure-related input | Why it matters |
|---|---|
| Available steam-supply pressure | Helps determine whether charging can occur at the required operating state |
| Expected fully charged pressure | Establishes part of the initial stored-energy condition |
| Minimum useful discharge pressure | Limits the portion of stored energy available to the process |
| Process-user pressure requirement | Defines the minimum acceptable pressure at the actual user |
| Distribution and control pressure losses | Affect the pressure required upstream of the process consumer |
| Vessel mechanical design pressure | Establishes a separate pressure-boundary design requirement under the governing code |
These values should be agreed through the responsible process and mechanical engineering teams.
The minimum pressure acceptable at a process user is not automatically the same as the minimum pressure required inside the accumulator.
A narrower useful pressure range may reduce the available discharge capacity and require reconsideration of the equipment arrangement.
Check Repeatability Rather Than One Successful Event
An accumulator that meets the first peak but begins each subsequent cycle with less stored energy may not provide sustainable support for the production schedule.
The supplier’s technical assessment should show the predicted charging and discharge behavior across the relevant repeated cycle.
It should also address the required steam quality, usable water inventory, steam space and the applicable limitations on steam release.
If the facility has a persistent generation deficit with no sufficient opportunity for charging, process scheduling changes, additional steam supply or another system-level solution may be necessary.
No universal energy-saving percentage or payback period can be guaranteed from the presence of an accumulator alone.
What Should Buyers Include in the Accumulator Equipment RFQ?
The Request for Quotation (RFQ) should connect the time-based steam requirement with the operating basis and the mechanical specification for the complete industrial pressure vessel.
Suppliers should be given enough information to understand the intended operating cycle and the boundaries of the proposed supply.
Include the Demand and Supply Evidence
| RFQ information | Required clarification |
|---|---|
| Steam-demand profile | Time-stamped mass-flow data for relevant operating cases |
| Data origin | Measured, calculated or estimated values, with limitations |
| Peak events | Magnitude, duration, overlapping consumers and repeated frequency |
| Available steam supply | Flow and pressure available for the defined service boundary |
| Recharge periods | Timing, duration and process constraints between peaks |
| Steam conditions | Applicable supply, charging and delivery pressure and temperature |
| Process requirements | Minimum acceptable user pressure and steam-quality expectations |
| Accumulator operating basis | Proposed charge/discharge cycle, initial conditions and operating limits |
| Mechanical design basis | Governing code and edition, design pressure and temperature, water conditions and cyclic duty |
| Equipment interfaces | Vessel connections, required associated equipment and system responsibilities |
| Quality documentation | Drawings, material records, inspection plan, examination and pressure-test requirements |
| Project delivery | Site conditions, transport restrictions, handling and installation boundaries |
| Open assumptions | Unverified process inputs, responsible parties and required technical dispositions |
Editorial RFQ template for complete industrial steam accumulator procurement. Final requirements depend on the project.
Separate Storage Performance From Vessel Manufacture
The technical and commercial documents should identify who is responsible for establishing the steam-system model, approving the pressure window, performing the storage-performance calculation and integrating the equipment into the existing network.
Mechanical vessel manufacture is a different responsibility from guaranteeing an entire steam system’s performance.
Depending on the contracted scope, a manufacturer may provide vessel engineering, fabrication and inspection documentation while process integration, associated controls and commissioning remain with the EPC contractor or other responsible parties.
Do not assume these additional services are included merely because a supplier manufactures pressure vessels.
For background on heavy-equipment manufacture, see the company’s pressure-vessel manufacturing overview. The proposed accumulator design, system interfaces and performance responsibilities must be confirmed for the actual enquiry.
Review Mechanical and Operational Acceptance Separately
For an applicable pressure-vessel project, the selected construction requirements may include ASME BPVC Section VIII or another specified framework, depending on the destination, design and contract.
The governing code and edition, material requirements, cyclic operating conditions and inspection documentation must be identified.
A completed manufacturing pressure test may demonstrate compliance with the applicable pressure-boundary test requirements. It does not, by itself, prove that the integrated accumulator system can support the site’s repeated steam-demand cycle.
Buyers should request a clear explanation of how the proposed capacity and operating envelope relate to the provided steam-demand profile.
A preliminary or budgetary enquiry may use clearly identified assumptions. Final design and fabrication release should follow the approved project technical basis.
Frequently Asked Questions
How do I calculate steam consumption for an accumulator assessment?
For an existing plant, use suitable steam-flow measurements where possible and organize them into a time-stamped load profile. For a planned process, consumption may be estimated from heat duties, relevant steam enthalpy differences and the operating schedule. In both cases, the critical requirement is to establish how demand changes over time, not only the total steam consumption for a day.
Can an hourly steam-demand report be used for accumulator sizing?
It may help establish overall consumption, but an hourly average may conceal short demand peaks that are important to accumulator selection. The appropriate recording interval should reflect the process events and be agreed by the responsible engineering team. Higher-resolution information may be needed.
Does the difference between peak demand and boiler capacity determine accumulator volume?
No. A flowrate difference must be considered over its duration and evaluated against the actual steam supply, permissible pressure window, stored-water condition, charging capacity and repeated operating cycle. Converting a steam-mass shortfall directly into vessel volume would omit essential thermodynamic and mechanical design considerations.
Conclusion
A reliable industrial steam accumulator assessment starts with a time-based record of steam demand and available supply.
Peak magnitude, duration, overlapping consumers and repeated operating cycles must be considered together with the charging opportunity and useful pressure range. Without those inputs, the apparent steam-storage requirement may be incomplete or misleading.
For a chemical plant steam-storage enquiry, provide the measured or clearly labeled estimated demand profile, actual available steam conditions, minimum required delivery pressure, repeated cycle, operating limitations and project equipment requirements. These data form the basis for assessing a complete industrial pressure vessel and defining the responsibilities for steam-system integration.
References
- Spirax Sarco. Steam Accumulators. The Boiler House — Learn About Steam. Technical explanation of demand peaks, charging, discharge, pressure conditions and accumulator sizing. https://www.spiraxsarco.com/learn-about-steam/the-boiler-house/steam-accumulators
- Spirax Sarco. Measurement of Steam Consumption. Steam Engineering Principles and Heat Transfer. https://www.spiraxsarco.com/learn-about-steam/steam-engineering-principles-and-heat-transfer/measurement-of-steam-consumption
- Spirax Sarco. Methods of Estimating Steam Consumption. Steam Engineering Principles and Heat Transfer. https://www.spiraxsarco.com/learn-about-steam/steam-engineering-principles-and-heat-transfer/methods-of-estimating-steam-consumption
- ASME. BPVC Section VIII, Division 1 — Rules for Construction of Pressure Vessels. Official public scope and standard listing; the full standard has not been reviewed for this article. https://www.asme.org/codes-standards/find-codes-standards/bpvc-viii-1-bpvc-section-viii-rules-construction-pressure-vessels-division-1