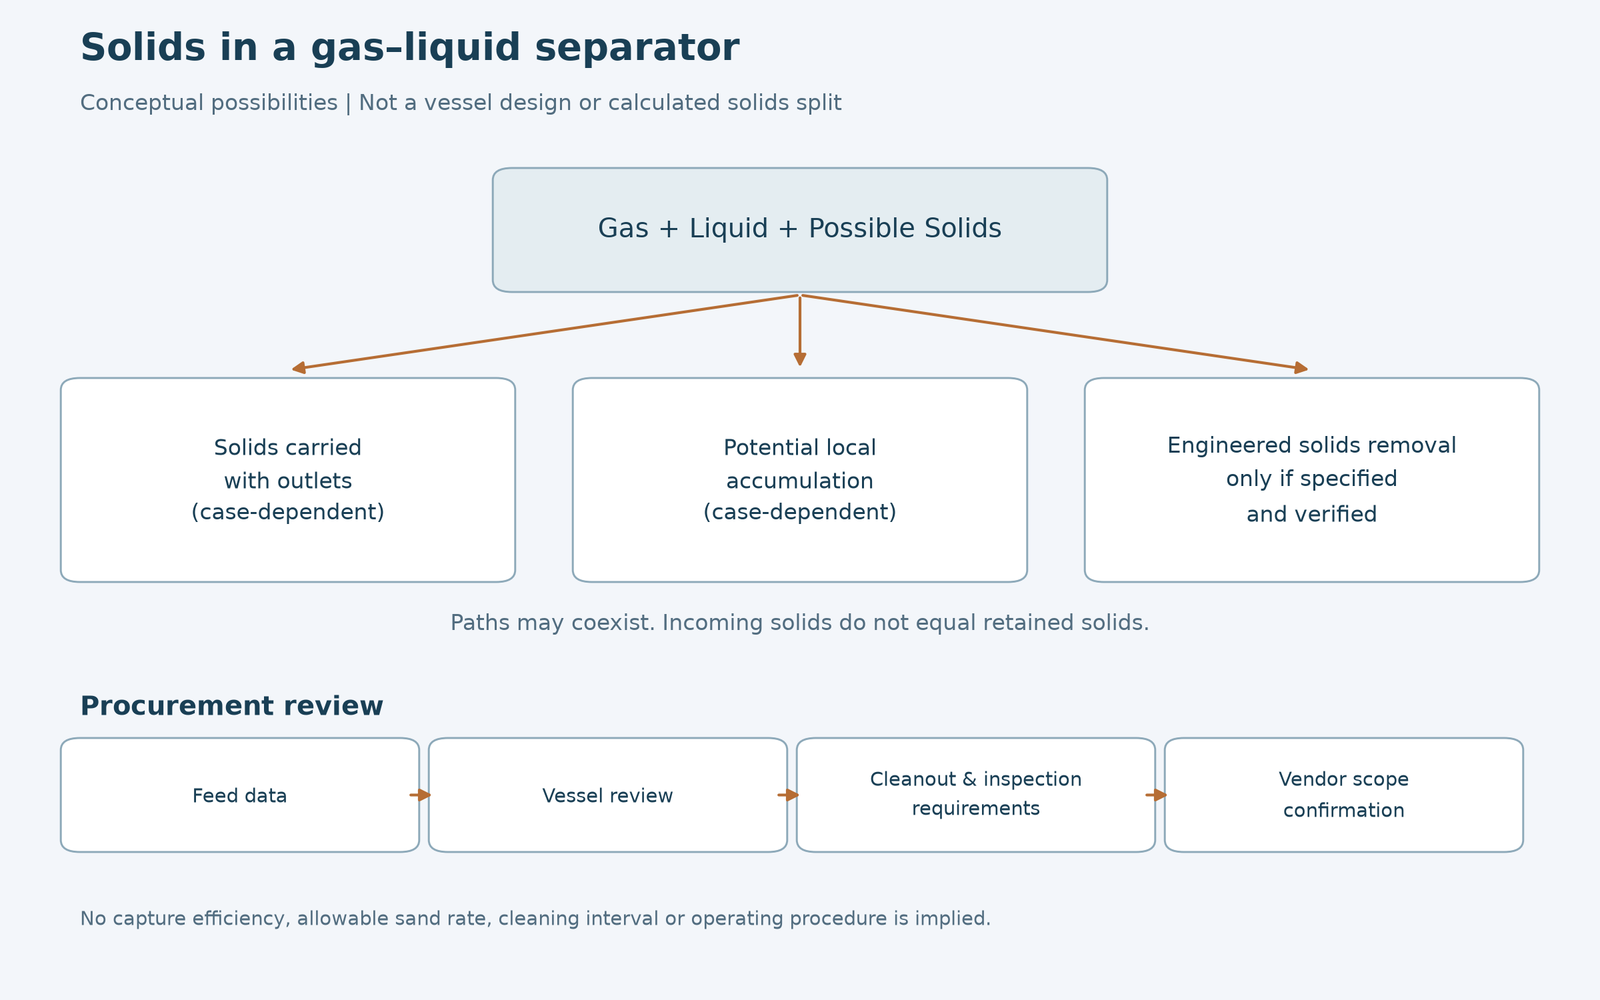
A gas–liquid separator may be designed to separate gas from liquid under a defined flow and pressure range. But when the feed also contains sand, corrosion products, scale or other solid particles, a conventional separator datasheet may not tell the complete procurement story. Some particles may leave with the liquid, some may be carried onward, and some may settle inside the vessel. The actual distribution depends on the feed, particle characteristics, flow regime and equipment design.
For gas–liquid separator solids handling, buyers should specify not only the average solids concentration, but also particle properties, intermittent peak loading, event duration, expected accumulation, cleanout access and the limits of the manufacturer’s proposed supply. These inputs allow process engineers and the equipment supplier to determine what needs investigation before the complete industrial separator is ordered.
A conventional gas–liquid separator is not automatically a dedicated sand-removal unit. For example, SLB describes a particular family of conventional horizontal well-test separators as capable of accommodating small quantities of solids, especially in configurations with a sand-jet line. That statement concerns SLB’s own equipment; it is not a general performance guarantee for all separators or for another manufacturer.
This guide is written for industrial owners, EPC process and equipment engineers, and buyers preparing a new separator enquiry. It covers specification and scope clarification, not pressurized sand-discharge procedures, operating instructions or stand-alone solids-removal equipment selection.
1. Why Does Solids Handling Need a Separate Review in a Gas–Liquid Separator RFQ?
A two-phase gas–liquid separator is generally assessed against gas and liquid feed rates, fluid properties, operating pressure and temperature, separation objectives, and control requirements. A three-phase vessel may have additional liquid–liquid separation and interface-control requirements. The presence of solids introduces a further question: what happens to the solid material over time?
The answer is not necessarily that every particle settles or that every particle leaves the vessel. Depending on its size, density, behavior and the local flow field, a particle may be transported with the exiting streams, deposited in relatively quiet regions, or redistributed during a process upset.
Accumulation can matter even when the average concentration appears low. Deposits may occupy space intended for liquid handling, affect drain or instrument connections, obstruct access to internal areas, or complicate the planned maintenance strategy. Abrasive particles can also contribute to localized erosion where their velocity and impact conditions are unfavorable. These are potential design concerns, not proof that a specific vessel will suffer a particular failure.
SLB’s public solids-management overview emphasizes that both the nature of incoming solids and the timing of their arrival matter to system design. Separately, the Society of Petroleum Engineers’ discussion of separator level measurement and flow assurance identifies sand and other deposits as possible sources of level-instrument reliability problems.
Separate the three questions often mixed together
| Procurement question | What the engineering team must establish | What must not be assumed |
|---|---|---|
| Can the vessel perform the specified gas–liquid separation duty? | Feed conditions, phase properties and required outlet quality for the defined operating cases | That a successful gas–liquid duty demonstrates a specified solids-removal efficiency |
| Will solids accumulate, and where might that matter? | Particle characteristics, transient input, operating levels and proposed vessel arrangement | That all incoming solids will either settle completely or leave with the liquid |
| Can the proposed complete equipment be inspected and cleaned as required? | Access concept, expected deposit locations, maintenance constraints, interfaces and responsibilities | That the existence of a drain or access opening proves a particular cleaning method will work |
Buyer takeaway: treat solids handling as an explicitly reviewed part of the overall separator service. If the feed data are incomplete, the supplier’s assumptions and technical exclusions must remain visible in the quotation.
2. Which Solids Data Should Be Included in the Separator Enquiry?
A useful enquiry distinguishes how much solid material arrives, what that material is like, and under which operating conditions it arrives. A statement such as “some sand may be present” leaves the supplier unable to determine a defensible service boundary.
State concentration, loading rate and the measurement basis
At minimum, provide the available values or clearly mark them as unknown:
- Solids concentration: Specify the actual reported unit and whether the basis is mass or volume. A value stated as ppm must identify its basis; mass-based ppm and volume-based ppm are not interchangeable.
- Reference phase: Identify whether a concentration refers to the liquid phase, total multiphase feed or a separately sampled slurry. Do not merge unlike sampling bases.
- Solids mass or volume flow: Provide a rate where it is measured or can be derived from validated phase flow and concentration data on consistent bases.
- Normal and maximum conditions: Show the average, representative operating range and anticipated episodic peaks separately.
- Confidence and sampling method: Identify sample location, collection period, analysis method, and limitations such as poor representativeness during a short sand event.
Concentration alone is not a mass-loading rate. Two operations with similar measured concentration may bring different total quantities of solids into the vessel because their liquid flowrates or event durations differ. Likewise, a brief intense event and a continuous low-level input can create different accumulation and maintenance concerns.
Characterize the particles beyond “sand”
The following properties may influence the process assessment and proposed equipment configuration:
| Solids attribute | Information the buyer should provide | Why it matters for review |
|---|---|---|
| Particle-size distribution | Available size distribution or relevant laboratory measurements, not just one nominal diameter | Different fractions may be transported, deposited or entrained differently |
| Particle density and composition | Mineral or chemical identification and available density data | Affects relative settling behavior and material compatibility assessment |
| Particle shape and abrasiveness | Descriptions or tests relevant to angularity, hardness or erosive potential | Helps the engineer assess potential localized wear, without implying a universal erosion rate |
| Adhesion and agglomeration | Evidence of sticky solids, deposits, agglomerates, wax-associated particles or other binding behavior | May affect deposition, obstruction and removal feasibility |
| Corrosive or reactive constituents | Available analysis of associated salts, water chemistry and process contaminants | May alter the materials and integrity assessment |
| Variability | Differences between normal samples, startup periods, production changes and upset conditions | Prevents a nominal sample from representing the entire service |
Do not assume that two feeds with the same particle-size distribution behave alike if their liquid viscosity, chemistry and phase conditions differ.
Supply the gas and liquid operating basis
The solids data must be reviewed alongside the process datasheet. The relevant information typically includes:
- Gas and liquid flowrates across minimum, normal, maximum and credible transient cases, stating actual or standard reference conditions as appropriate.
- Gas and liquid composition, density and viscosity information, including changes with pressure and temperature where relevant.
- Operating and design pressures and temperatures, with the project code basis defined by the responsible engineer.
- Gas–liquid ratio, expected liquid slugs and changes in flow regime, where applicable.
- Liquid foaming, emulsions, wax, scale, high viscosity or other characteristics that may influence separation or deposits.
- Desired gas and liquid outlet specifications and any process constraints that influence the complete vessel design.
The owner or EPC process team should define and approve the process information. The manufacturer should review the resulting specification only within the agreed scope of engineering responsibility.
3. How Should Intermittent Sand or Solids Peaks Be Described?
An average concentration does not describe a peak event. In oil-and-gas and industrial process service, solids may arrive unevenly during well cleanup, changes in upstream equipment, restarts or other service-specific disturbances. These are possible sources of variation, not a prediction for every plant.
To make transient loading reviewable, define the event rather than substituting a larger average value.
Describe each credible operating scenario
| Scenario | Data to submit | Main issue for vendor clarification |
|---|---|---|
| Normal continuous service | Representative solids concentration and gas/liquid flow profiles | Whether the proposed arrangement accommodates the stated routine service and expected accumulation |
| Short-duration solids peak | Peak concentration or loading rate, duration, coincident fluid flows and frequency | Whether transient deposits, restrictions or other limits require additional evaluation |
| Start-up or restart condition | Known initial state, expected phases, solids observations and transient flows | Whether deposits already present or sudden loading changes affect the proposed design assumptions |
| Upstream change or process upset | Defined credible deviation, available measurements, expected sequence and duration | What the supplier has included or excluded from its design review |
| Extended operation between maintenance windows | Expected operating time, total anticipated solids input and historical deposit evidence | Whether access and maintenance planning remain practical under the selected arrangement |
This matrix is an editorial RFQ structure, not an equipment performance rating. No numerical peak capacity, allowable solids load or cleaning interval should be assigned without relevant test or operating evidence and an approved engineering basis.
Separate rate, duration, frequency and cumulative quantity
A technically useful record should make four dimensions clear:
- Instantaneous or interval loading: How much solid material arrives per unit time at the specified conditions?
- Event duration: How long is the elevated loading expected to last?
- Event frequency: How often might such events recur during the relevant project period?
- Accumulation and removal assumptions: What evidence supports an estimate of retained solids, and what fraction may leave with the normal outlet streams?
An inferred accumulation quantity requires a defensible retention basis. It must not be assumed to equal all solids entering the vessel. Any modeled value should identify uncertainty, relevant process cases and the responsible reviewer.
What if solids data are not available?
Do not replace missing data with an invented typical sand concentration or an unspecified “minor solids” allowance.
Instead, the EPC can issue a clarification register recording:
- The unknown quantity and which project party owns it.
- Available upstream or historical evidence.
- Whether a sampling or characterization plan has been approved by the process owner.
- Any provisional design assumption, clearly labeled as unverified.
- The supplier’s written qualification or exclusion until the information is resolved.
- The decision stage at which the assumption must be confirmed before procurement or final design approval.
This makes the uncertainty manageable without presenting a guess as a guaranteed design condition.
4. How Can Solids Accumulation Affect Vessel Layout, Controls and Cleanout?
A separator’s solids-handling evaluation is not confined to the gas outlet and separation efficiency. It also concerns the space occupied by deposits, how the plant can observe potential accumulation, and whether the vessel can be maintained within the operating philosophy.
Effective space and deposit location
In some arrangements, settled solids may reduce the volume available for liquid handling or create local obstructions. The actual impact depends on geometry, liquid level range, flow distribution, particle behavior and deposit locations. It should be assessed rather than assumed.
The process and equipment teams should clarify whether significant deposits could affect:
- Normal liquid level or interface measurement.
- Access to instrument tappings and associated connections.
- Liquid outlet or drain arrangements.
- Internal flow paths, distribution elements or maintenance access.
- The inspection coverage needed at likely wear or deposit locations.
The SPE technical discussion on level-measurement reliability provides useful context for why deposits and solids should be considered when planning instrumentation interfaces.
Cleanout provisions are part of the complete equipment review
Before ordering, the buyer and project engineers should agree on the required cleanout outcome and maintenance concept, rather than choosing an internal arrangement solely because it appears in another supplier’s brochure.
Questions to resolve include:
- Will the intended maintenance philosophy require a planned shutdown for cleaning, and how will the plant prepare the vessel for safe access under its approved procedures?
- What locations need inspection or cleaning access, based on the engineering assessment of likely accumulation?
- Does the equipment layout leave practical access to the areas and interfaces that need attention?
- What handling, isolation, waste-management and site constraints must be addressed by the owner and EPC?
- Are any cleanout connections, internal features, instruments or other interfaces included in the complete vessel quotation, or excluded for separate engineering?
- Who is responsible for confirming the effectiveness of a proposed arrangement and its maintenance documentation?
The existence of a manway, drain or flushing provision is not proof of a particular removal efficiency. Equally, a statement that a unit has “sand handling” capability is inadequate without a defined feed basis and service limitations.
As a real third-party example, SLB’s Conventional Horizontal Separator product sheet describes certain well-test separator configurations that accommodate small quantities of solids and may include a sand-jet line for cleaning. This does not mean that those provisions are automatically suitable, necessary or supplied for every industrial gas–liquid separator.
Inspection and integrity implications
Where solids may be abrasive, deposit-forming or chemically aggressive, the qualified engineering team should consider the potential for localized damage or difficult-to-access inspection locations. The actual damage mechanism, materials, inspection requirements and interval cannot be inferred from sand concentration alone.
A buyer may request an inspection-access review, but the final inspection strategy and any in-service integrity decisions belong to the owner and authorized specialists under applicable requirements.
5. What Must the Complete-Separator Supplier Confirm in Writing?
For a new separator, the quotation should demonstrate how the offered equipment relates to the buyer’s approved duty. An unqualified statement such as “solids tolerated” leaves major responsibilities undefined.
Distinguish confirmed design capability from proposed options
| Clarification topic | Owner/EPC input | Required supplier response |
|---|---|---|
| Intended duty | Gas–liquid or gas–liquid–liquid service, flow cases and outlet requirements | Description of the complete offered separator and performance assumptions |
| Solids characteristics | Concentration basis, load rate, particle distribution, composition, relevant variability | Explicit solids service basis used in the review; unknowns and limitations |
| Intermittent conditions | Event rate, duration, recurrence and coincident fluids | Statement of which transient cases were reviewed or excluded |
| Accumulation | Historical deposits, likely maintenance window and open process questions | Assumptions about deposition and whether a separate assessment is required |
| Access and cleanout | Site maintenance philosophy, space and operating constraints | Included access features, interfaces, exclusions and responsibilities |
| Mechanical integrity | Approved design conditions, applicable codes and materials requirements | Defined design/fabrication scope and documents, subject to project approval |
| Inspection and documents | Project inspection philosophy and document register | Offered drawings, inspection/test documentation and unresolved submissions |
| Performance statements | Proposed acceptance criteria and test basis, if any | Measurable guarantees only for conditions and tests expressly agreed in the contract |
| Supply boundary | Battery limits, site works and responsibilities | Included equipment, separate packages, buyer-supplied items and deviations |
This is a procurement clarification matrix, not a declaration that the manufacturer provides specialized desanding technology, on-site servicing or independent process engineering.
Do not confuse vessel construction compliance with solids capacity
An applicable pressure-vessel construction code addresses the pressure-containing equipment within its scope. That does not automatically certify a solids collection rate, a cleaning frequency or a separator outlet-solids specification.
For relevant oil-and-gas separators, API RP 12J:2024 is titled Process Design of Oil and Gas Separators and Scrubbers. Its publicly available scope distinguishes conventional separation elements from more specialized solids handling arrangements, which depend on project or technology-specific requirements. The paid standard has not been reproduced or independently applied as a design calculation in this article.
The project must confirm which codes, editions and regulatory requirements apply to its actual equipment and destination. A certificate or a cited design standard does not replace a documented process suitability assessment.
Clarify the battery limits
The proposal should identify what the vessel manufacturer is supplying as part of the complete industrial separator, including the agreed pressure boundary, relevant internal arrangement, integrated connections, access provisions and deliverable documentation.
If the project requires upstream solids conditioning, external solids collection, waste handling, instrumentation packages, site piping, automation or special cleaning systems, those requirements need explicit ownership and interface definition. This article is not a recommendation to purchase any of those items separately from the company.
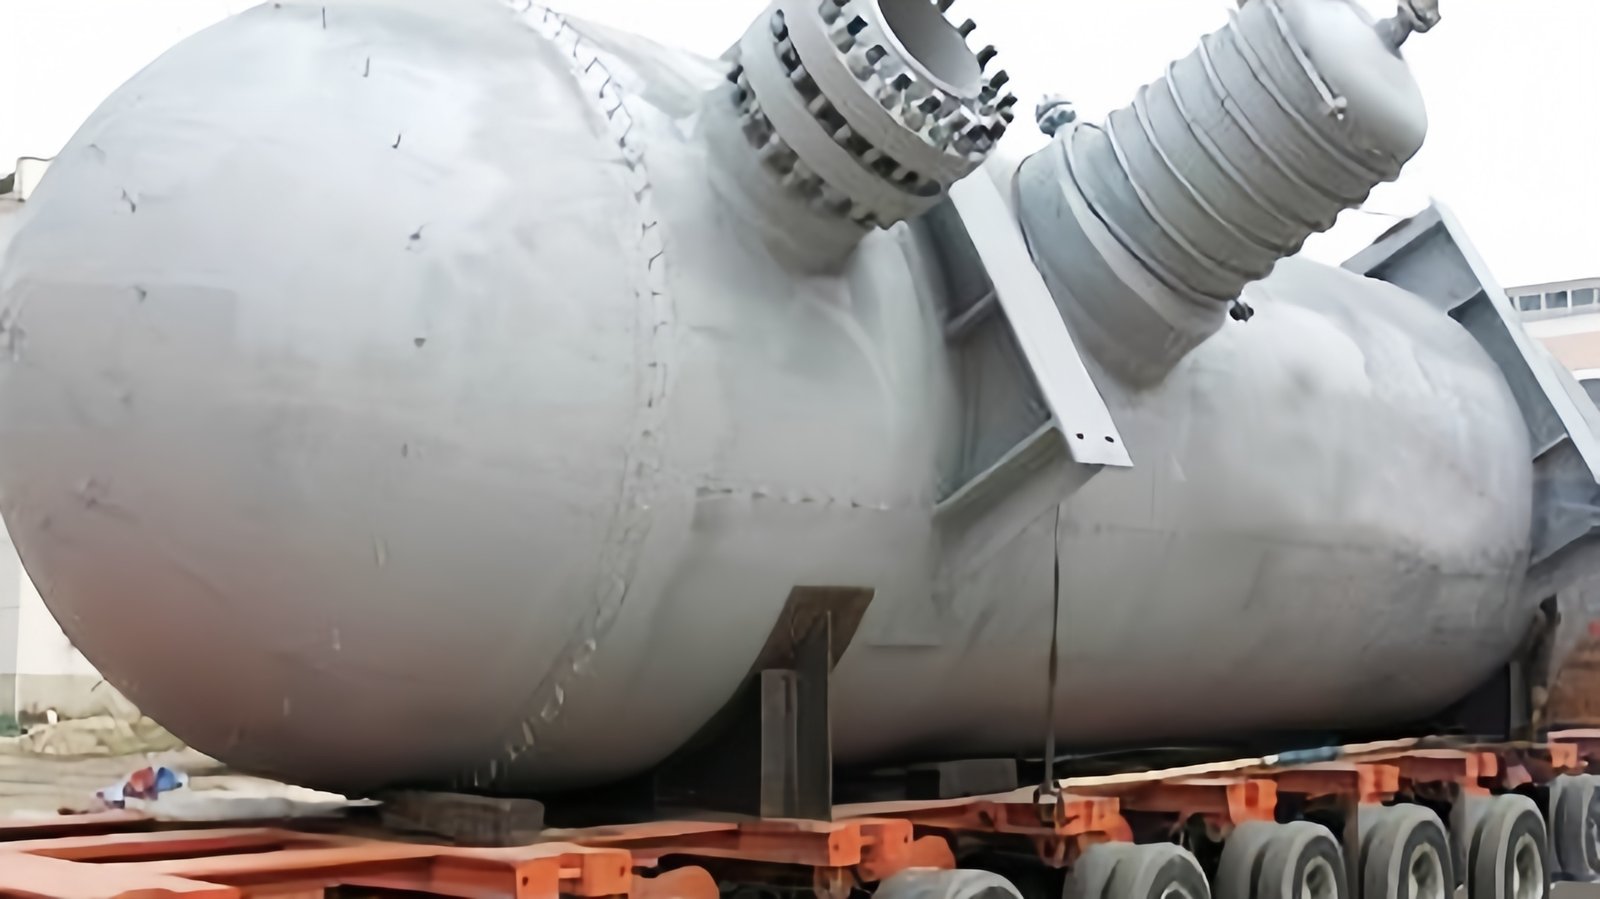
A manufacturing capability shown on a refining-industry pressure-vessel project page demonstrates relevant industrial equipment experience. It does not independently establish a guaranteed high-sand separator rating or the availability of every specialized solids-removal arrangement.
6. What Should Be Included in a Gas–Liquid Separator Solids-Handling RFQ Package?
The purpose of an RFQ data package is to make the supplier’s assumptions and scope auditable before the commercial offer is accepted.
Owner/EPC data checklist
| RFQ item | Required information or status | Primary responsibility |
|---|---|---|
| Project and vessel duty | Location, service description, gas–liquid or three-phase basis, process objective | Owner / EPC process |
| Flow and thermodynamic basis | Minimum/normal/maximum and credible transient gas and liquid conditions; units and reference bases | EPC process |
| Solids quantity | Representative concentration, correct unit and phase basis, relevant solids flowrate | Owner / EPC process |
| Solids characteristics | Particle-size distribution, density, composition, hardness/abrasiveness and adhesion tendency where known | Owner / process/materials specialists |
| Transient solids events | Peak rate, duration, frequency, coincident fluid conditions and uncertainty | Owner / EPC process |
| Operating and maintenance philosophy | Planned maintenance windows, cleaning expectations and applicable site constraints | Owner / operations |
| Historical evidence | Sampling, deposition, obstruction, wear or other relevant plant records | Owner / operations / reliability |
| Mechanical basis | Design pressure/temperature, materials basis, code and required documentation | EPC mechanical / materials |
| Inspection and access | Required access review, inspection interfaces and site constraints | EPC mechanical / inspection |
| Battery limits | Included whole vessel, instrument and site interfaces, excluded packages | EPC / procurement |
| Vendor deviations | Written assumptions, limitations, optional features and unresolved technical questions | Separator supplier |
| Review and approval | Responsible technical reviewers and outstanding decision gates | Owner / EPC |
A supplier should not be expected to prove missing feed characteristics from a generic product description. Where important data are unavailable, list the uncertainty and agree on the path for resolving it.
Questions worth putting directly into the technical bid evaluation
- What exact solids concentration and loading basis was used to evaluate the offered separator?
- Does the assessment cover the specified peak events and their durations, or only nominal continuous operation?
- Which particle characteristics were assumed, and what changes would require re-evaluation?
- Does the proposed equipment incorporate any provision for anticipated deposits, and what assumptions support that provision?
- Which access and cleanout interfaces are included in the complete vessel supply?
- What site cleaning, waste-handling, instrumentation or specialist systems are excluded?
- Have potential impacts on liquid levels, instrumentation, outlets and relevant inspection locations been reviewed within the agreed scope?
- Which stated performance requirements, if any, are contractually guaranteed, and under what defined conditions and acceptance basis?
- What information must the EPC provide before the proposed design is finalized?
- Who approves the process assumptions, mechanical design, maintenance philosophy and final equipment acceptance?
These questions make competing offers more comparable without suggesting a fabricated maximum sand content, separator capacity, cleaning cycle or numerical solids-removal efficiency.
Turn the answers into an approved engineering boundary
Before placing an order, the owner/EPC should record:
- Confirmed inputs supported by drawings, operating data or relevant characterization.
- Engineering assumptions that still require review.
- Supplier inclusions and exclusions described in unambiguous contract language.
- Technical deviations and the party authorized to accept them.
- Unresolved risks requiring an assessment before detailed design or manufacture.
- Required deliverables for the complete pressure vessel and its agreed interfaces.
For an equipment enquiry, the industrial pressure-vessel product overview can provide context on the manufacturer’s broader equipment categories. Buyers should then submit the actual feed conditions and RFQ documents through the contact page for a project-specific discussion of complete equipment and confirmed supply scope.
Frequently Asked Questions
Does a conventional gas–liquid separator automatically remove all incoming solids?
No. A conventional separator is primarily specified for its gas–liquid separation duty. Depending on particle behavior and the equipment’s arrangement, some solids may leave in the outlet streams while others accumulate. A guaranteed solids-removal duty requires an explicit technical basis and agreement, not an assumption based on the vessel’s name.
Can one solids concentration limit be applied to every separator?
No. The applicable limits depend on the gas and liquid conditions, particle properties, transient loading, geometry, process requirements and proposed maintenance arrangement. An advertised value from one manufacturer’s model cannot be transferred to another design without qualification.
Why is peak solids loading important if the average concentration is low?
A short event may bring material into the separator at a different rate than normal operation. Its consequences depend on the quantity arriving, event duration, frequency, fluid conditions and where material may deposit or pass through. Buyers should describe these scenarios separately rather than relying on an average alone.
Which particle data matter most to a separator buyer?
Useful inputs include measured concentration with units and sampling basis, particle-size distribution, density, composition, potential abrasiveness, adhesion or deposit-forming behavior, and variability between operating conditions. The responsible engineers should decide which properties require further characterization.
Does adding a cleanout connection guarantee trouble-free operation?
No. A connection or access opening is only one part of a site-specific maintenance and vessel design concept. The intended deposit locations, access feasibility, safe isolation arrangements, waste handling and responsibilities must be reviewed and documented by the appropriate project team.
Who is responsible for confirming solids-handling performance?
The owner and EPC normally define and approve the feed and process requirements. The equipment supplier should state what it has evaluated and what is included in its agreed scope. Any specified performance guarantee, test basis or responsibility split must be established in project documents rather than inferred from a general product brochure.
Is API RP 12J a guarantee that a separator can remove sand?
No. API RP 12J concerns the process design of applicable oil-and-gas separators. Meeting relevant project standards does not automatically create a numeric solids-removal guarantee or establish the capability of a separate specialized cleaning or solids-management system.
Conclusion
A gas–liquid separator RFQ is incomplete when solids are described only as “some sand” or a single unqualified concentration value.
Buyers should define the solids amount and measurement basis, particle characteristics, average and transient loading, relevant gas and liquid conditions, potential accumulation, access and cleaning requirements, and the boundaries of the proposed complete equipment. The supplier should then provide a written response identifying the engineering cases considered, uncertainties, scope and exclusions.
This evidence-based approach helps EPC teams compare industrial separator offers without assuming that conventional gas–liquid separation automatically delivers complete solids removal. It also makes clear where additional process data, qualified review or a different system-level arrangement may be needed before the equipment is ordered.
References
- SLB. Conventional Horizontal Separator (product sheet, copyright 2011). Public example of a specific well-test separator that can accommodate small quantities of solids, with cleaning features in some configurations. Its specifications and capabilities must not be attributed to other manufacturers. https://www.slb.com/-/media/files/testing-services/product-sheet/conventional-separator-ps.ashx
- SLB. Solids Management. Manufacturer’s public overview explaining why solids characteristics and the timing of solids arrival matter to production-system design. https://www.slb.com/products-and-services/innovating-in-oil-and-gas/well-production/processing-and-separation/solids-management
- Society of Petroleum Engineers, Journal of Petroleum Technology. The Savvy Separator: Oil/Water Separation and Gas Processing Facilities—Impact of Process Flow Conditions on Level Measurements. Technical discussion of deposit and solids impacts on level-measurement reliability. https://jpt.spe.org/the-savvy-separator-oil-water-separation-and-gas-processing-facilities-impact-of-process-flow-conditions-on-level-measurements
- American Petroleum Institute. API RP 12J:2024—Process Design of Oil and Gas Separators and Scrubbers, Ninth Edition. Public publisher/catalog information about the standard’s scope; the full paid standard was not consulted. https://www.api.org/products-and-services/standards/digital-catalog
- BSI Knowledge. API RP 12J:2024 (public standard-description and edition page). Scope of the pressure-vessel-based gas–liquid and gas–liquid–liquid separation recommended practice. https://knowledge.bsigroup.com/products/process-design-of-oil-and-gas-separators-and-scrubbers-ninth-edition