A gas cooler can meet its specified heat duty and pressure-drop target on paper while leaving an important question unanswered: what happens when the process gas carries abrasive particles through the exchanger? A purchase specification based on gas flow, inlet and outlet temperatures, and a preferred alloy may not describe the local impact and corrosion conditions that determine whether the complete exchanger is suitable for service.
For EPC teams and industrial equipment buyers, the practical issue is not to choose an allegedly erosion-proof material. It is to establish a traceable connection between particle data, gas-side operating cases, possible condensation, equipment geometry, assessment evidence, and the supplier’s actual scope. This guide focuses on large, complete gas-cooling heat exchangers and the information required before a technically comparable RFQ can be issued.
Procurement takeaway: Define the solids reaching the exchanger inlet, not only the solids leaving an upstream process; pair those solids data with the gas state for each credible case; and ask bidders to explain their wear and corrosion assessment, limitations, inspection access, and remaining uncertainties. Neither a pressure test nor a material grade alone proves resistance to long-term erosion-corrosion.
What Does Erosion-Corrosion Mean in a Particle-Laden Gas Cooler?
The term erosion-corrosion is sometimes used loosely for any metal loss in a flowing process stream. In an engineering review, the potential damage mechanisms should be considered separately before their interaction is assessed.
| Potential mechanism | Main question for the buyer | Why the distinction matters |
|---|---|---|
| Solid-particle erosion | Can entrained particles repeatedly strike exposed surfaces and mechanically remove material? | Particle characteristics, local trajectories and impact conditions matter; an aggressive chemical environment is not required for mechanical erosion. |
| Corrosion | Could the actual process environment chemically or electrochemically attack the selected materials? | Gas composition, temperature, deposits and any resulting liquid phase may govern the corrosion environment. |
| Erosion-corrosion interaction | Could flow or particle impacts damage protective surface films or expose fresh metal in a corrosive environment? | An assessment of erosion alone or corrosion alone may not capture their combined effect. |
This is a damage-mechanism screening framework, not a diagnosis of a particular failure. Deposits, localized overheating, fabrication conditions, vibration, and other mechanisms may also contribute to degradation. The responsible materials or integrity specialist must evaluate the credible mechanisms for the service.
The ASM Handbook chapter Failure Analysis of Heat Exchangers identifies erosion-corrosion among several forms of exchanger degradation. A peer-reviewed review of corrosion in heat exchangers describes the interaction between fluid motion and corrosion processes. These references provide technical background; neither establishes a safe operating threshold for an unidentified gas-cooling project.
Why Is Changing the Alloy Alone Not a Complete Solution?
An alloy may provide improved resistance to a defined corrosive environment, but it does not independently determine how particles enter the exchanger, where they strike, or how much of the gas-side surface is exposed to repeated impacts. Conversely, a mechanically erosion-resistant surface may still need review for the actual process chemistry and fabrication requirements.
A complete evaluation connects at least four questions:
- What arrives? Particle loading, size distribution, mineral or chemical composition, shape, hardness where relevant, and realistic variation in upstream separation performance.
- How does it move? Gas density and flow, exchanger-side assignment, inlet and internal geometry, local acceleration, turning and flow distribution, and possible deposition or re-entrainment.
- What environment exists at the surface? Gas chemistry, temperature, deposits, and whether cooling can create a corrosive liquid film or condensate.
- What can be demonstrated? The assessment method, approved assumptions, relevant experience or testing, accessible inspection locations, and contractual acceptance boundary.
A published study of solid-particle erosion at the tube-sheet end of a shell-and-tube exchanger found that the location of affected tubes was sensitive to the modeled particle size and inlet flow conditions. This is a useful illustration of local flow dependence, not a transferable erosion-rate equation for every industrial gas cooler. See Habib et al., International Journal for Numerical Methods in Fluids.
Avoid a single-number shortcut: A nominal gas velocity, alloy name, corrosion allowance, or heat-transfer area cannot by itself establish acceptable wear, service life, or inspection frequency. Those conclusions require a project-specific, agreed assessment.
Which Particle Data Should the EPC Team Supply Before an RFQ?
Start with the solids expected at the gas-cooler inlet nozzle. An upstream process description such as “dusty gas” or “contains catalyst fines” is a warning, not an adequate design basis. Data taken before a cyclone, filter, reactor outlet, or process mixing point may not represent the population that actually reaches the exchanger.
Record particle loading on a declared basis
Report particle concentration with units and its measurement or calculation basis. If the basis is a standard or normal gas volume, state the reference temperature, pressure, and wet/dry definition. If reporting a mass ratio or a solids mass flow, state the corresponding gas mass flow, time basis, and conditions. A number in mg/Nm³ without the reference conditions and sampling point can be difficult to compare with another data source.
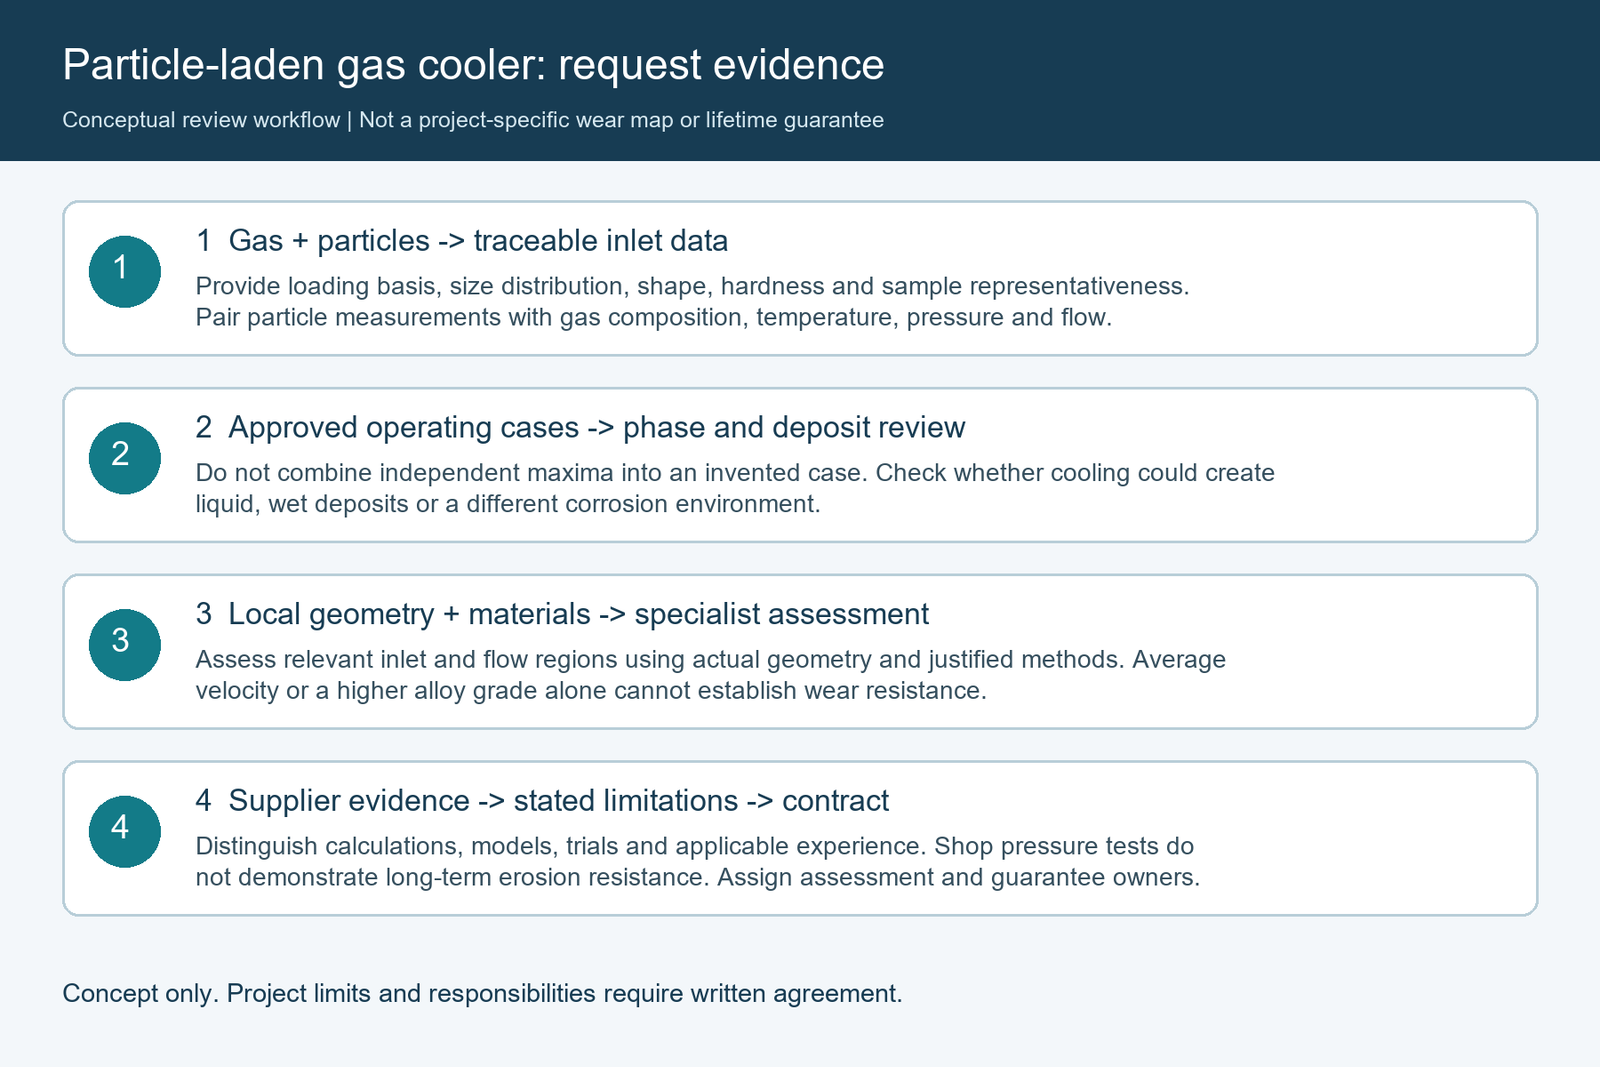
Ask whether the reported value represents a time average, a short excursion, a measured peak, or a design allowance. The plant’s process engineer should identify which conditions are simultaneously credible; do not combine unrelated maxima into a fictional worst-case operating point.
Provide a size distribution, not only an average size
A useful particle analysis identifies the particle-size distribution, its measurement method and basis (for example, a reported mass-based rather than number-based distribution), and any known coarse-particle tail or agglomeration. The supplier may need more detail than a single mean diameter to investigate impingement and deposition. The appropriate reporting format depends on the characterization method and the model to be used.
Where available, also identify:
- Particle composition or mineralogy; whether the material is coke, ash, catalyst, mineral dust, or another substance.
- Relevant hardness, shape or angularity information, and particle density or other properties required by the assessment method.
- Stickiness, agglomeration, friability and potential for deposit formation or particle break-up.
- Whether upstream equipment can shed occasional larger debris or change the particle population during credible disturbances.
- Sampling location, date, operating state, analytical method, uncertainty and whether the sample represents normal or limiting service.
Not every field can be known at the first inquiry. Mark missing values as “To be confirmed” and agree on who will obtain them. Do not populate a generic particle size or an assumed dust concentration merely to complete the vendor datasheet.
A minimum particle-evidence register
| RFQ field | Buyer-provided information | Evidence or status to record |
|---|---|---|
| Solids identity | Composition/mineralogy and potential contaminants | Analysis or approved process description; revision |
| Particle loading | Concentration or mass rate, units and wet/dry or reference-volume basis | Sample/model source and operating case |
| Particle size | Distribution and measurement basis, including relevant coarse tail | Laboratory method and representative sample ID |
| Physical behavior | Shape, hardness/density where relevant, agglomeration or deposition behavior | Test result, engineering judgment or explicit gap |
| Upstream separation | Equipment boundary and expected effectiveness under relevant conditions | Responsible supplier’s stated basis; no assumed efficiency |
| Sampling location | Point relative to upstream separation and exchanger inlet | P&ID reference and location |
| Variability | Normal and credible upset or short-duration peak states | Duration, evidence, approval status |
Editorial data register for procurement coordination; it is not an industry-prescribed form or a set of mandatory numerical limits.
Pair Particle Data With the Same Gas-Cooling Operating Cases
A dust analysis is only useful when it can be mapped to a gas state and exchanger duty. A nominal hourly flow and an independent “maximum solids” number may not occur at the same time. Equally, a seemingly modest average gas flow says little about the local particle trajectories in a particular inlet chamber or flow passage.
For each approved case, record gas mass flow, composition, inlet temperature and pressure, outlet target, allowable gas-side pressure drop, particle loading/distribution, and utility conditions. Include the proposed phase state, especially if condensate is possible. The process team should confirm which cases are physically credible and which are merely screening sensitivities.
| Case to evaluate | Coupled gas and particle information | Key exchanger question | Approval status |
|---|---|---|---|
| Normal production | Normal gas state, measured/approved particulate profile, cooling utility | Can the proposed exchanger meet thermal and hydraulic requirements while addressing the identified mechanisms? | Owner/EPC to approve |
| High gas-throughput case | Corresponding—not automatically maximum—particle loading, gas density and pressure | Do the specified inlet and local flow conditions warrant additional wear assessment? | Confirm simultaneous conditions |
| High-solids case | Actual gas flow, particle distribution, peak duration and upstream equipment state | Where might solids impinge or deposit, and what evidence supports the review? | Validate representative peak |
| Low flow or turndown | Particle behavior at the approved turndown gas state | Could reduced transport, deposition or subsequent re-entrainment affect the design? | Include only credible case |
| Cooling/condensation boundary | Gas chemistry, cold-side condition, dew-point/phase assessment and particle state | Could wet deposits, liquid films or changes in the flow regime alter corrosion or fouling exposure? | Process phase assessment required |
| Approved upstream change or disturbance | Linked particle and gas data, event duration and operating permission | Does the change fall outside the equipment’s assessed service envelope? | Owner/EPC change review |
These are candidate case labels, not authorization for any plant to operate under an upset. Process safety, operating permission and applicable protections remain the responsibility of the project and site engineering authorities.
Could cooling create a different corrosion environment?
Yes, depending on the composition and temperature/pressure path. A gas that is dry at the inlet may develop condensate on or near colder surfaces, potentially changing the chemical environment in which particles and deposits contact metal. Some streams may remain single-phase over the entire approved envelope. Neither conclusion can be assumed from the name “gas cooler.”
The EPC process team should provide a suitable phase-equilibrium/condensation assessment where this risk exists, including relevant corrosive constituents, condensate chemistry if known, temperature range, and drainage or downstream handling boundary. Wet-gas conditions must not be silently inferred from a dry-gas analysis, or vice versa.
For the basic gas composition, outlet condition, pressure drop and condensate-interface requirements, see our separate gas-cooler heat exchanger specification guide. This article adds the particle-impact and damage-assessment layer; it does not repeat the complete general gas-cooling RFQ.
Which Parts of the Exchanger Need a Localized Assessment?
A shell-and-tube exchanger contains changes in flow direction, available area and local geometry. Depending on the selected configuration and fluid assignment, a particle-laden gas may interact differently with inlet nozzles, distribution regions, tube entrances, baffle zones, return bends and outlet passages. These locations are items to review, not a claim that every design has the same damage pattern.
The inquiry should ask bidders to identify the actual configuration used in the review and explain why it is appropriate for the specified gas and particle envelope. Where particle impacts are credible, that explanation may include a justified flow-distribution study, a particle-trajectory or localized wear assessment, operating references with comparable conditions, or further specialist evaluation if reliable evidence is unavailable.
An Alfa Laval transfer-line exchanger brochure discusses coke-particle erosion in a specific hot cracked-gas application. It demonstrates that solids carried by gas can affect heat-exchanger design and reliability. The brochure’s proprietary design features and performance assertions do not establish the correct solution for another gas cooler or the capabilities of WSHI.
A practical review should ask:
- Is the proposed gas-side allocation and configuration supported by the stated particle and thermal data?
- Which locations may experience concentrated impacts, deposition or difficult-to-inspect metal loss?
- How were local flow distribution, operating pressure drop and heat-transfer performance assessed together?
- What happens to the assessment when the particle distribution or condensation state changes?
- Can the specified inspection or cleaning locations actually be accessed with the offered equipment and plant layout?
Avoid specifying a stand-alone protective insert, coating, or tube component as the procurement objective. Any proposed protection must be evaluated as part of the complete exchanger design, including its effects on mechanical integrity, pressure drop, thermal duty, examination and maintenance.
What Evidence Should a Supplier Return With the Technical Bid?
A claim such as “erosion-resistant design” is not an acceptance method. Request a clearly identified assessment package that matches the agreed service cases and distinguishes assumptions from demonstrated findings.
| Bid evidence | What should be stated | Limitation or clarification to resolve |
|---|---|---|
| Approved service basis | Revision-controlled gas, particle and utility cases; assumptions and exclusions | Which missing data were supplied by the vendor rather than approved by EPC? |
| Thermal/hydraulic rating | Heat duty, outlet condition and gas/utility pressure losses for stated cases | Does the model include any relevant phase change and deposition assumptions? |
| Geometry and flow review | Actual gas path, nozzles, flow distribution and regions assessed | Is local assessment required beyond bulk-average velocity? |
| Particle/wear assessment | Method used, particle properties, boundary conditions and results, where contractually required | Is the model validated or only a screening estimate? What is outside its applicability? |
| Corrosion/materials basis | Expected corrosion environment, selected materials and supporting basis | Are wet or deposited conditions credible and considered? |
| Inspection and maintenance concept | Access provisions, proposed inspection locations and relevant documentation | Can the owner verify service condition after commissioning? |
| Mechanical QA and tests | Applicable code, material traceability, NDE and pressure/leak-test scope | These establish specified mechanical requirements, not erosion life. |
| Deviation and open-item register | Every unresolved input, responsible party and decision milestone | What must be resolved before contractual performance wording is fixed? |
Evidence strength matters. A preliminary engineering calculation may screen options; a computational model may examine a defined local flow arrangement; relevant operational history or representative testing may offer additional support. None should be represented as a validated service-life guarantee unless the contractual method, input data and supporting validation actually justify that conclusion.
For comparable equipment construction and fabrication considerations, review the manufacturer’s shell-and-tube heat exchanger product page. Public manufacturing capability descriptions are not a substitute for a confirmed project-specific wear-analysis or process-performance service.
Who Owns the Data, Assessment, Manufacturing and Acceptance Boundaries?
Before comparing prices, the project should allocate responsibilities explicitly. A conventional exchanger fabricator and a process technology provider may have different scopes, even if both submit technical information during the same procurement process.
| Workstream | Typical lead for definition or approval | Required interface or record |
|---|---|---|
| Actual gas and particulate envelope | Process owner/EPC with upstream process specialists | Approved process data, operating-case register, sample basis |
| Condensation and corrosive-service assessment | EPC process and materials specialists | Property model, chemistry and approved service envelope |
| Required local erosion assessment | Party identified by purchase scope, with specialist review as needed | Method, inputs, assumptions, validation limitations and deliverables |
| Thermal and mechanical exchanger proposal | Exchanger designer/supplier within its contracted scope | Rating, drawings, material selection basis, deviations |
| Fabrication, examination and pressure-boundary QA | Equipment manufacturer and designated inspectors | Material and manufacturing records, inspection/testing dossiers |
| Installed monitoring, inspection strategy and operating changes | Owner/operator and appointed integrity team | Access provisions, monitoring plan, change-control records |
| Performance or service-life guarantee | Only the explicitly contracted responsible party | Measurable conditions, limitations, method and remedy provisions |
This is a proposed allocation for clarification, not a representation that the website’s equipment manufacturer supplies every listed service. Confirm the signed supply scope and responsible engineers for the actual project.
Why is a shop pressure test insufficient as erosion evidence?
A pressure or leakage test may demonstrate that a manufactured pressure boundary meets specified mechanical acceptance requirements at the test conditions. It does not reproduce a plant’s particle loading, gas chemistry, impact locations, temperature history or accumulated exposure. Therefore, it cannot independently establish acceptable long-term erosion, corrosion or remaining wall life.
If the purchase contract includes operating-performance or damage-resistance commitments, the buyer and responsible technical parties must first agree on the case definition, supporting evidence, measurement or inspection method, acceptance criteria and exclusions. Avoid declaring a universal safe gas velocity, guaranteed zero metal loss, or inspection interval without those project inputs.
Particle-Laden Gas Cooler RFQ: Copyable Buyer Checklist
The following fields can be included in the technical inquiry or attached as a particle-specific supplement to the main gas-cooler datasheet. They are not mandatory values from a standard.
| Field | Information to provide or request | Status/owner |
|---|---|---|
| Equipment identification | Complete industrial gas-cooling exchanger; service, tag and location | EPC |
| Coupled operating cases | Normal and approved limiting gas/particle conditions; case duration | Process owner/EPC |
| Gas composition and state | Components, wet/dry analysis, mass flow, inlet/outlet T/P and gas phase | EPC process |
| Gas-side ΔP limit | Allowable pressure drop, named measurement boundary and case | EPC process |
| Utility conditions | Cooling medium quality, temperature/flow range and constraints | EPC utilities |
| Solids concentration | Units, mass/volumetric basis, gas reference conditions, sampling point | Process/upstream specialist |
| Particle distribution | Size distribution and method, composition and relevant physical traits | Sampling/analysis owner |
| Data representativeness | Sampling dates, upstream equipment states, variability and gaps | EPC process |
| Credible peaks/transitions | Particle loading, gas state, permitted case and duration together | EPC approval |
| Condensation/corrosion | Phase assessment, corrosive constituents, deposit/wet-zone risks | EPC process/materials |
| Configuration proposal | Gas side, nozzles, geometry and maintenance access | Exchanger bidder |
| Local wear evidence | Screening or specialist analysis method, input and limitation register | Bidder or appointed specialist per scope |
| Mechanical construction | Applicable code/edition, materials, inspections and tests | EPC/mechanical supplier |
| Service access | Inspectable zones, access and cleaning scope where applicable | Bidder/owner |
| Supplier boundaries | Included/excluded engineering, monitoring and downstream systems | Commercial/technical bid |
| Acceptance and guarantees | Agreed case, proof method, exclusions, owner and unresolved items | Contractual parties |
Suggested RFQ sentence: “Quote the complete gas-cooling heat exchanger against the attached revision-controlled gas and particle operating cases. State the gas-side arrangement and methods used to review localized particle impact and relevant corrosion conditions. Identify missing input data, unsupported cases, inspection limitations and exclusions explicitly. Do not treat mechanical pressure testing as evidence of erosion service life.”
How Should Buyers Compare Competing Offers?
First, verify that all bidders have assessed the same approved operating cases. One offer based on clean dry gas and another based on a particulate-bearing wet case cannot be ranked by surface area or price alone. A lower assumed dust load, a missing peak event or an optimistic upstream separation assumption can materially change the evaluation basis.
Second, compare assessment transparency rather than a headline promise. Does each bidder identify the local regions considered, which geometry was analyzed, which properties were measured versus estimated, and what needs confirmation? A proposal supported only by a generic alloy description is not equivalent to a documented, relevant review—even if both mention erosion resistance.
Third, confirm the full installed and acceptance scope. Include required access for inspection, agreed drawings, technical dossiers and the responsibilities for upstream separation, site monitoring and downstream interfaces. Do not assume that changing the component material solves missing process data.
A nearby topic on heat exchangers for slurry service addresses particle handling in a liquid-carried solids stream. Those considerations are not automatically interchangeable with a gas carrying entrained particles; phase behavior, transport and impact conditions require their own review.
Frequently Asked Questions
Does changing to a higher alloy grade eliminate gas-side erosion?
No. Alloy suitability depends on the specific corrosion and mechanical wear conditions. Particle size and loading, local gas paths, operating states, condensation behavior and inspection strategy still require engineering review. An alloy change may be part of an approved solution, but it is not an independent guarantee against particle impacts.
What particle information is most important in a gas cooler RFQ?
At minimum, identify what solids reach the exchanger inlet, their loading and measurement basis, particle-size distribution, relevant composition and physical properties, and which operating cases those measurements represent. Missing information should be visible and assigned to an owner rather than replaced by assumed numbers.
Is there a universal safe gas velocity for a particle-laden exchanger?
No single value is appropriate for all particle/gas/material/geometry combinations. The responsible designer must assess the specified service and local flow conditions using an agreed method. A generic bulk velocity does not describe all potential impact locations.
Can a factory pressure test prove erosion-corrosion resistance?
No. Pressure-boundary tests address defined mechanical acceptance conditions, not the long-term effect of gas-borne particle impacts and potentially corrosive environments. Any durability claim needs project-specific technical justification and an explicit contractual basis.
Conclusion: Specify the Evidence, Not an Unsupported Lifetime
For a particle-laden gas-cooling project, a defensible procurement decision begins with representative particles, matched gas operating conditions, a credible condensation assessment, and a documented review of local flow and material exposure. These inputs allow the responsible engineering parties to identify where assessment, monitoring access or further testing is needed.
Ask suppliers to return their calculation or study basis, known limitations, actual equipment and inspection scope, and unresolved technical points. That produces a more meaningful comparison of complete industrial heat exchangers than choosing an alloy or assuming an erosion life that nobody has demonstrated.
For a project-specific scope discussion, provide the process data, solids analyses, current P&IDs and required review boundary when requesting a quote for a custom shell-and-tube heat exchanger.
References and Engineering Reading
- ASM International. Failure Analysis of Heat Exchangers, ASM Handbook, Volume 11A (2021). General exchanger failure-analysis and corrosion-mechanism background; not a project design approval.
- Habib, M. A., et al. Solid-particle erosion in the tube end of the tube sheet of a shell-and-tube heat exchanger, International Journal for Numerical Methods in Fluids (first published 2005). Specific research on particle size, inlet conditions and localized erosion; not a universal wear model.
- Faes, W., et al. Corrosion and corrosion prevention in heat exchangers, Corrosion Reviews. Review discussion of corrosion and erosion-corrosion interactions across exchanger duties; contextual guidance only.
- Alfa Laval. Transfer Line Exchangers. Manufacturer information on coke-particle exposure in a specialized hot-gas service. Product designs and claims are Alfa Laval’s and are not attributed to this site’s manufacturer.
Editorial note: All data matrices in this guide are templates for project clarification. Numerical acceptance limits, inspection intervals, material selections and design responsibilities must be confirmed against approved project information and the applicable contract.